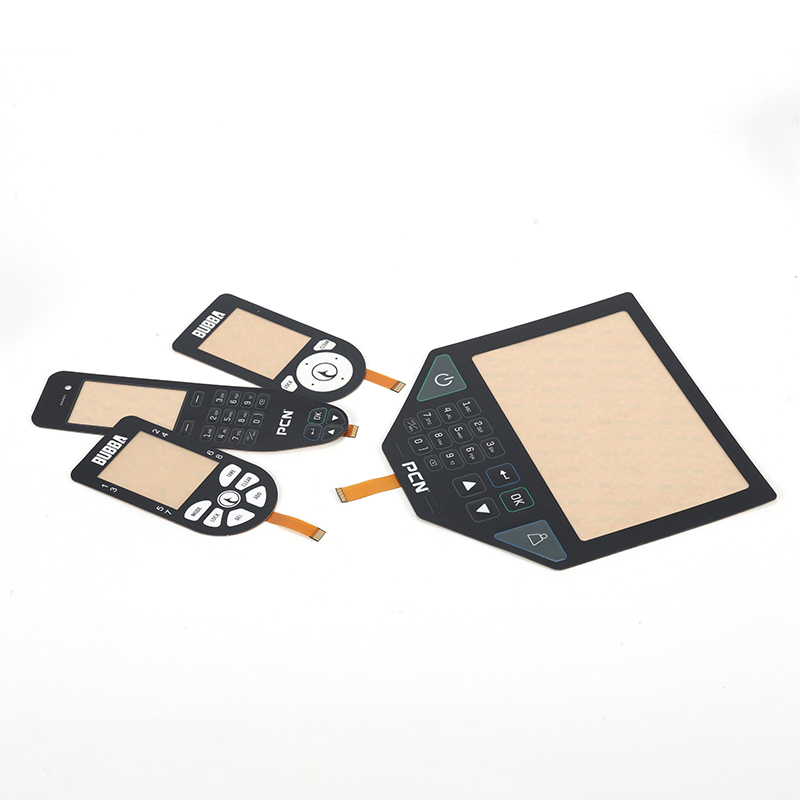
Customized FPC Membrane Switch with Shielding
High-density FPC circuit, integrated ESD shielding layer, custom actuation force, zero signal crosstalk.
Direct-from-factory custom membrane keypads, tactile dome arrays, ESD-shielded numeric matrices, and backlit user interfaces manufactured under strict ISO 9001 and Intertek-verified quality standards.
High-density FPC circuit, integrated ESD shielding layer, custom actuation force, zero signal crosstalk.
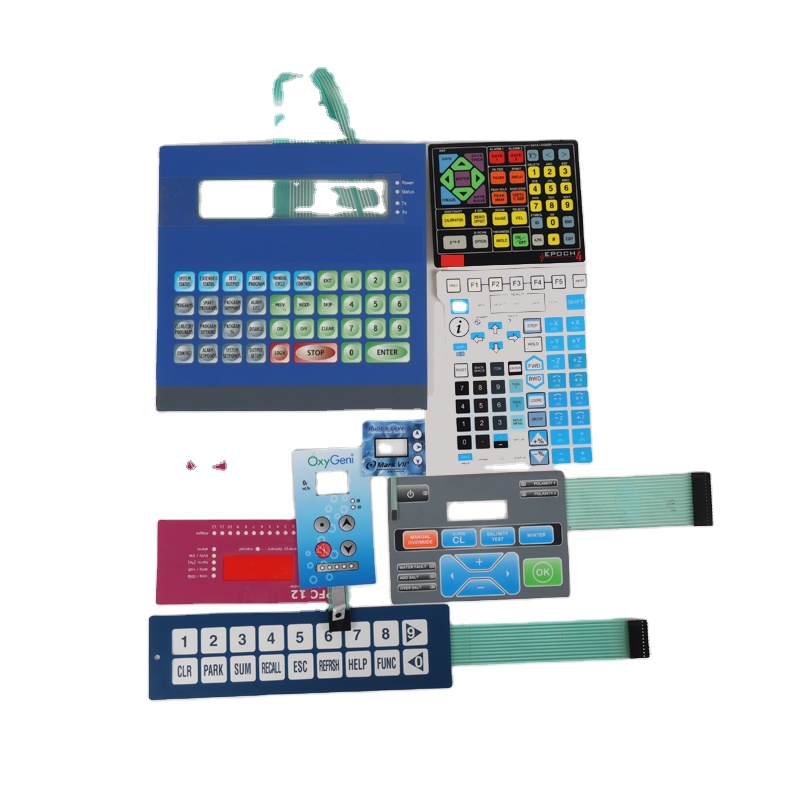
IP67 perimeter seal, stainless steel metal domes, crisp snap ratio, premium 3M adhesive backing.
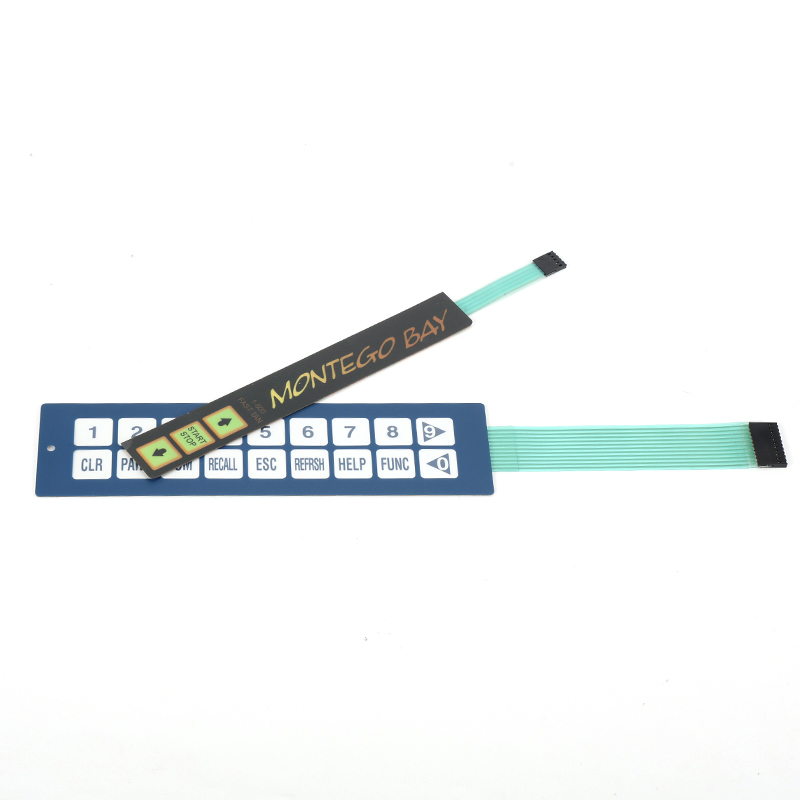
Engineered for >1,000,000 actuations, chemical-resistant PET overlay, anti-glare finish.
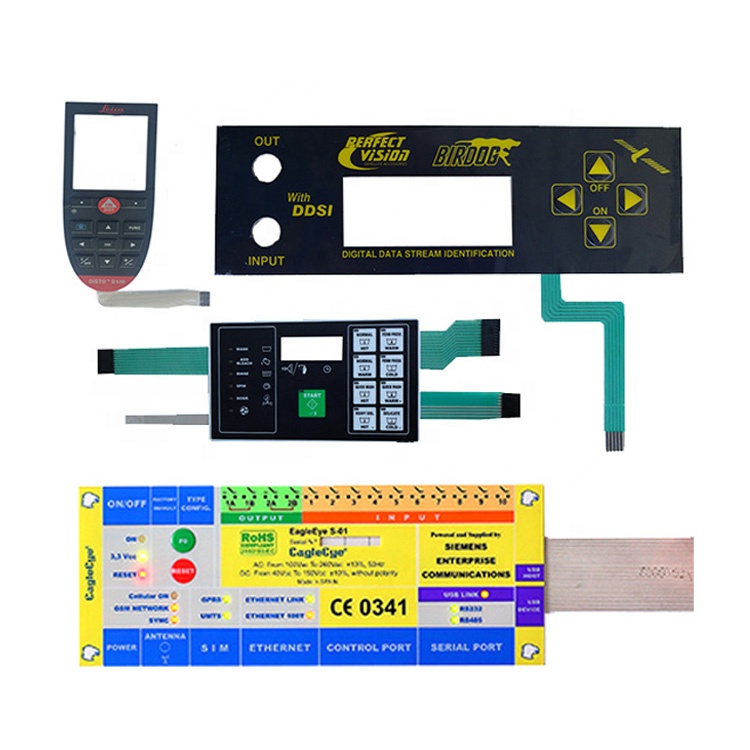
Ruggedized poly-dome/metal-dome layout, vibration proofing, extreme thermal tolerance (-40°C to +85°C).
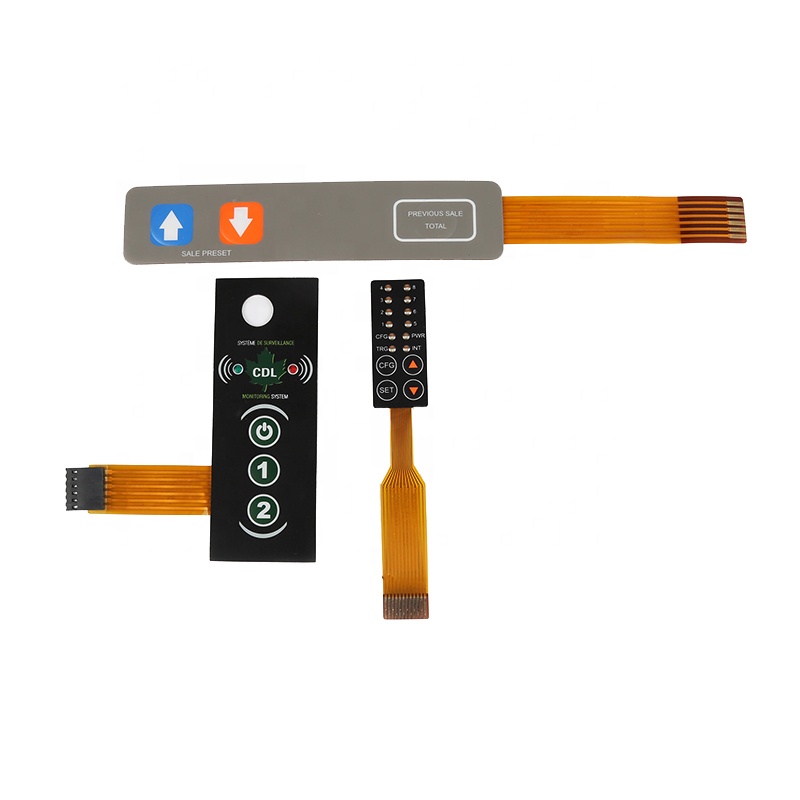
Solid-state ITO touch sensing, zero mechanical wear, seamless wipe-down cleanability for medical labs.
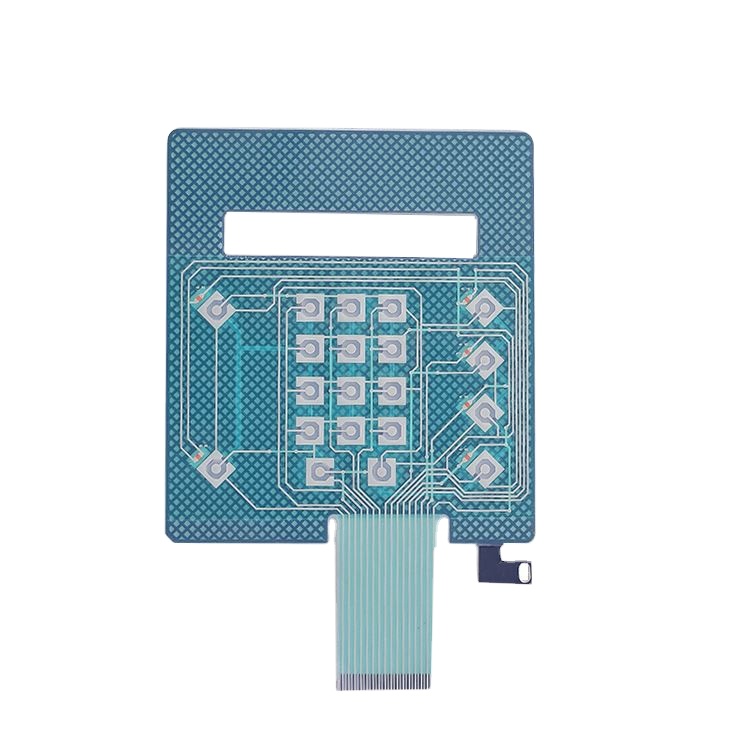
Full aluminum/printed silver grounding mesh protecting internal ICs against >15kV static discharge.
Light Guide Film (LGF) technology, low power consumption, selective backlighting for low-light operations.
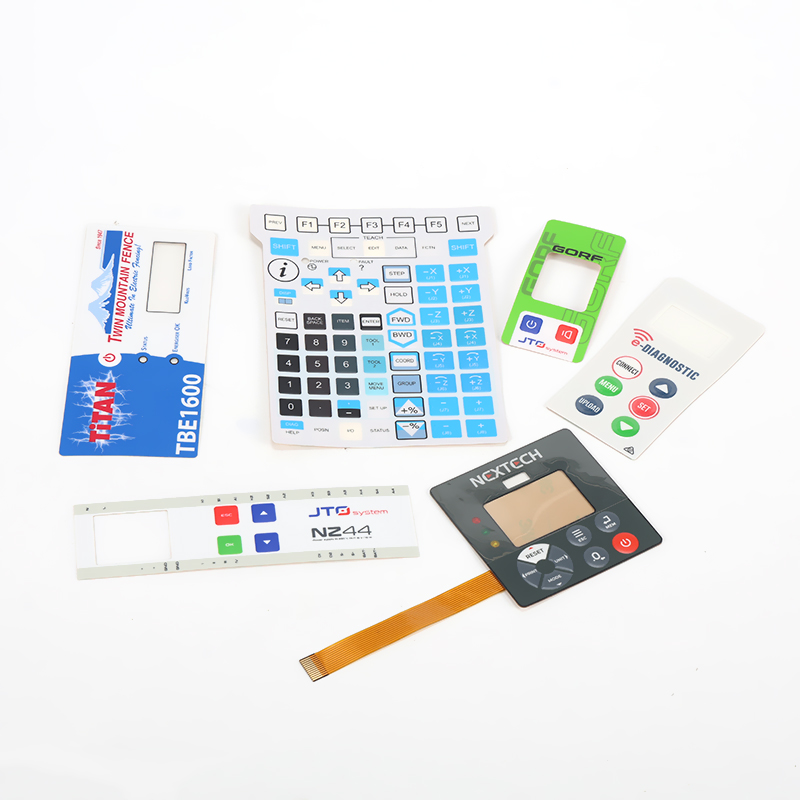
NEMA 4X / IP68 compliant design, UV-stable materials, resistance to industrial oils, solvents, and fuels.
In the heart of Silicon Valley, Santa Clara stands as a global epicentre for high-density electronic hardware design, advanced semiconductor fabrication tooling, bio-medical equipment, and industrial automation. For hardware design engineers, systems integrators, and procurement directors operating across Great America Parkway, San Tomas Expressway, and Mission College Boulevard, selecting a reliable membrane numeric keypad factory & supplier requires a rigorous evaluation of electromagnetic compatibility (EMC), dielectric strength, tactile force displacement consistency, and supply chain transparency.
As an established OEM/ODM pioneer founded in 1996, Zhejiang ZIRA Membrane Switch Co., Ltd. bridges the gap between high-spec Silicon Valley design engineering and direct-factory manufacturing scalability. With over 29 years of dedicated focus on human-machine interface (HMI) technology, a 5,000 m² cleanroom-equipped manufacturing campus, and verified Intertek audit standing, ZIRA delivers custom-engineered keypad solutions built to withstand the demanding operating parameters of Santa Clara’s technology sectors.
From cleanroom semiconductor processing tools to mobile robotic diagnostics, our membrane numeric keypads are optimized for mission-critical environment compliance.
Santa Clara host major semiconductor capital equipment innovators. In wafer processing, chemical vapor deposition (CVD), and photolithography sub-systems, input keypads must endure continuous exposure to aggressive solvents (isopropyl alcohol, acetone) and airborne particulate contamination. ZIRA manufactures Autotex XE textured PET overlays paired with sealed circumferential gasketing and conductive anti-static grounding meshes, preventing ESD discharge from damaging sensitive microcontrollers during high-speed wafer processing.
For medical device startups and established healthcare equipment vendors in the Santa Clara biomedical corridor, hygiene and sterile wipe-downs are non-negotiable. Our capacitive touch and embossed membrane numeric keypads incorporate antimicrobial film surface coatings and IP67 liquid-proof flush bezels. This eliminates bacteria-trapping crevices, enabling seamless sterilization with harsh medical disinfectants without legend degradation or false actuation.
Silicon Valley’s robotics and automated logistics equipment require input interfaces capable of handling continuous mechanical shock, intense vibration, and outdoor solar exposure. ZIRA utilizes high-grade stainless steel tactile metal domes (rated from 300g to 500g force) and UV-stabilized polycarbonate/polyester graphic films with 3M 468MP high-tack adhesive backing to guarantee zero delamination in mobile field environments.
Santa Clara is one of the highest-density data center markets in North America. Rackmount KVM switches, high-density server access panels, and power distribution units (PDUs) demand compact numeric input matrices with integrated LED status indicators. ZIRA customizes ultra-thin flexible printed circuits (FPC) with surface-mount 0603/0805 LEDs, enabling crisp backlighting in dark rack enclosures with low power draw.
Understand the multi-layer stack-up engineered by ZIRA to deliver long-term mechanical reliability, superior tactile feedback, and complete electromagnetic shielding.
| Performance Parameter | Autotex PET (Polyester) | Makrofol PC (Polycarbonate) |
|---|---|---|
| Flexural Fatigue Life | > 5,000,000 cycles | ~ 100,000 cycles |
| Chemical Resistance | Excellent (Alcohols, Acids, Solvents) | Moderate (Vulnerable to aromatic hydrocarbons) |
| Tensile Strength | Very High (Resists tearing) | High |
| Clarity / Transparency | High (Matte / Gloss / Selective texturing) | Water Clear (Ideal for thick display lenses) |
| Operating Temperature | -40°C to +85°C | -30°C to +105°C |
*ZIRA’s DFM engineering team assists Santa Clara clients in selecting the optimal material stack-up during pre-production prototyping.*
How next-generation HMI requirements are shaping custom membrane keypad manufacturing for Northern California OEMs.
Modern hardware designs are shifting from purely mechanical switches to hybrid capacitive touch surfaces. By printing Indium Tin Oxide (ITO) or conductive silver sensor loops behind glass or thick PET panels, OEMs achieve sleek, smartphone-like glass interfaces while retaining the low tooling cost and rugged durability of custom graphic overlays.
Traditional localized LED backlighting often results in uneven hot spots. Silicon Valley designers increasingly specify integrated Light Guide Film (LGF) layers. LGF redirects light from side-emitting surface-mount LEDs evenly across individual key legends, icon borders, and logo accents, dramatically reducing power consumption and stack-up thickness.
To accommodate complex microcontrollers, CAN-bus communication chips, and high-density connectors directly on the keypad switch assembly, OEMs are replacing traditional flexible PET screen-printed circuits with double-sided FR4 PCBs or Polyimide FPC substrates, creating a unified, plug-and-play HMI module.
Leverage three decades of proven manufacturing mastery, vertically integrated production, and rigorous third-party verified quality management.
Our factory facilities, legal operations, line capacity, and QA protocols are independently verified onsite by Intertek inspection auditors.
Every single matrix keypad undergoes automated continuity, contact resistance, dielectric breakdown, and loop resistance testing prior to shipment.
Send your AutoCAD DXF, SolidWorks, or Adobe Illustrator engineering files. Our R&D engineering team delivers DFM reviews within 24 hours.
Long-standing manufacturing partner to global industrial automation leaders including ABB and Emerson, exporting up to 50% of annual output worldwide.
Clear, direct answers regarding custom tooling, lead times, sample delivery, and technical specifications for Silicon Valley engineering teams.
For prototype engineering orders, standard lead time is 7 to 10 working days following final DFM artwork sign-off. Express air freight to San Jose International Airport (SJC) or San Francisco International Airport (SFO) typically takes 3 to 5 business days via DHL, FedEx, or UPS DDP services, allowing Santa Clara engineering teams to maintain rapid NPI (New Product Introduction) cycles.
Yes. While mass production orders typically range from 1,000 to 50,000 pieces, ZIRA fully supports Silicon Valley startups and pilot-stage OEMs with low Minimum Order Quantities (MOQs) starting from as few as 1 to 100 prototype units. Laser-cutting technology allows us to eliminate steel rule die tooling costs during early design iterations.
We integrate dedicated ESD grounding layers into the keypad stack-up. This involves screen-printing a continuous conductive silver grounding grid or laminating an aluminum foil shield directly beneath the graphic overlay layer. The shield routes static charges up to 15kV (Air Discharge) directly to the ground wire, shielding sensitive internal ICs and microprocessors.
To provide an itemized engineering quote within 24 hours, please supply: (1) Vector artwork for graphic overlay color matching (AI, PDF, or CorelDraw with Pantone/RAL color codes), (2) Mechanical dimensioned drawing (DXF, DWG, or STEP file), (3) Circuit schematic or pinout definition including tail length and connector part number, and (4) Special requirements such as metal dome tactile force, backlighting, or IP sealing ratings.
We use precision computer-controlled color matching systems synchronized with Pantone Matching System (PMS) and RAL color standards. All graphics are sub-surface screen-printed in dust-free cleanrooms. Display windows (for LCD or LED screens) can be left water-clear, tinted with transparent colors, or treated with selective anti-glare, scratch-resistant hardcoats.
All materials utilized—including PET films, polycarbonate sheets, silver/carbon conductive inks, SMT LEDs, and 3M structural adhesives—are 100% compliant with EU RoHS and REACH environmental standards. Our manufacturing system operates under ISO 9001:2015 quality management, and our facility profile is independently verified on-site by Intertek.
Partner directly with a primary membrane numeric keypad factory. Contact our senior HMI application engineers today for immediate DFM review, material stack-up recommendations, and custom sample production.
