Featured Industrial Waterproof Membrane Keyboards
Custom-fabricated tactile keypads, graphic overlays, and FPC/PCB assemblies engineered to withstand chemical washdowns, harsh UV, and extreme operating temperatures.
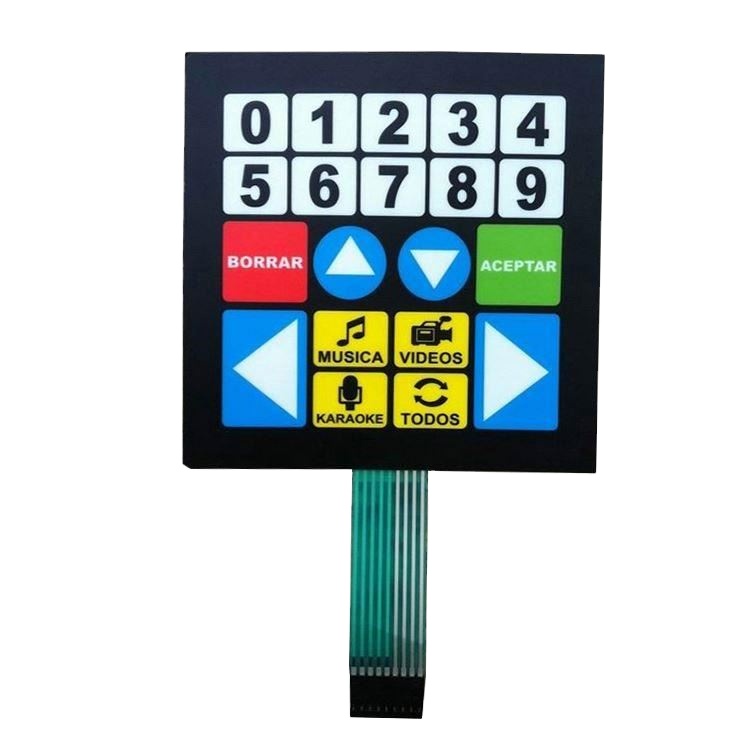
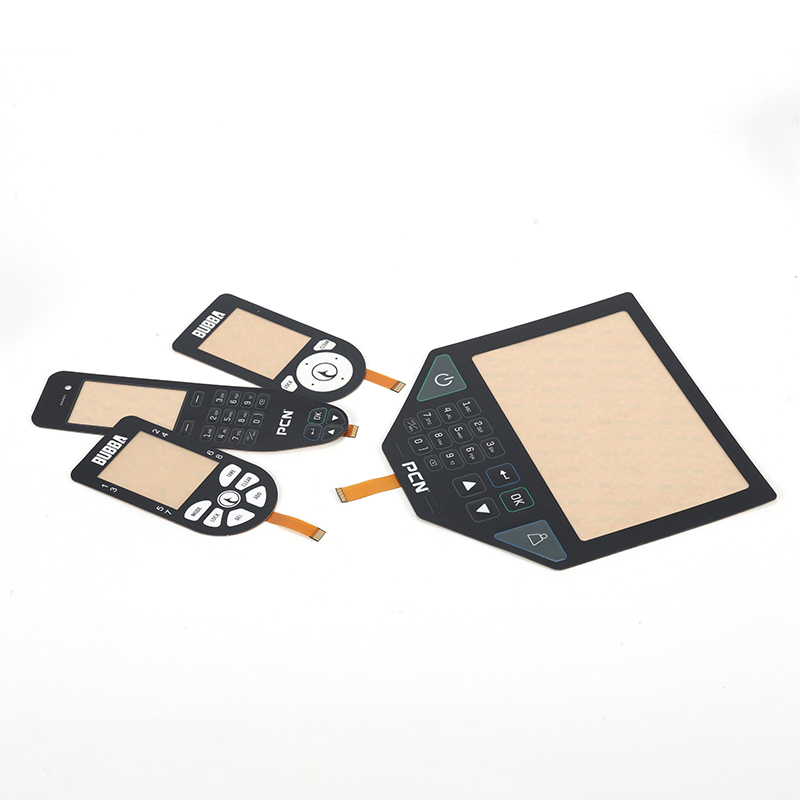
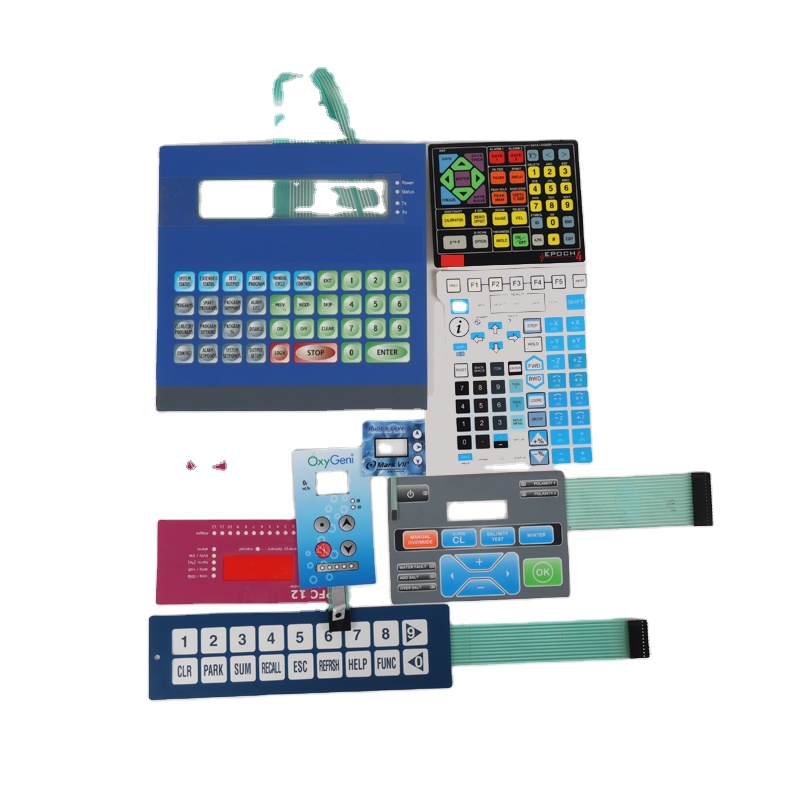
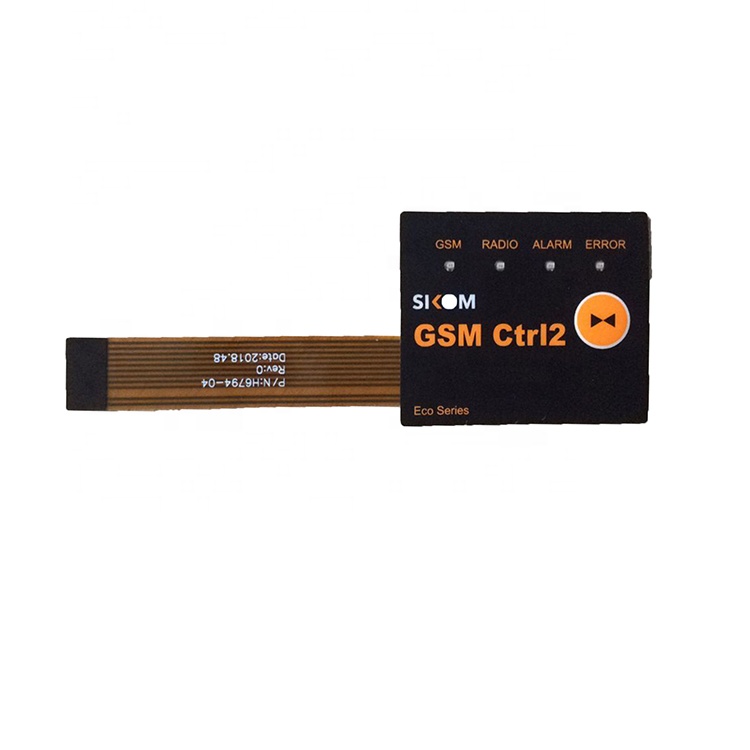
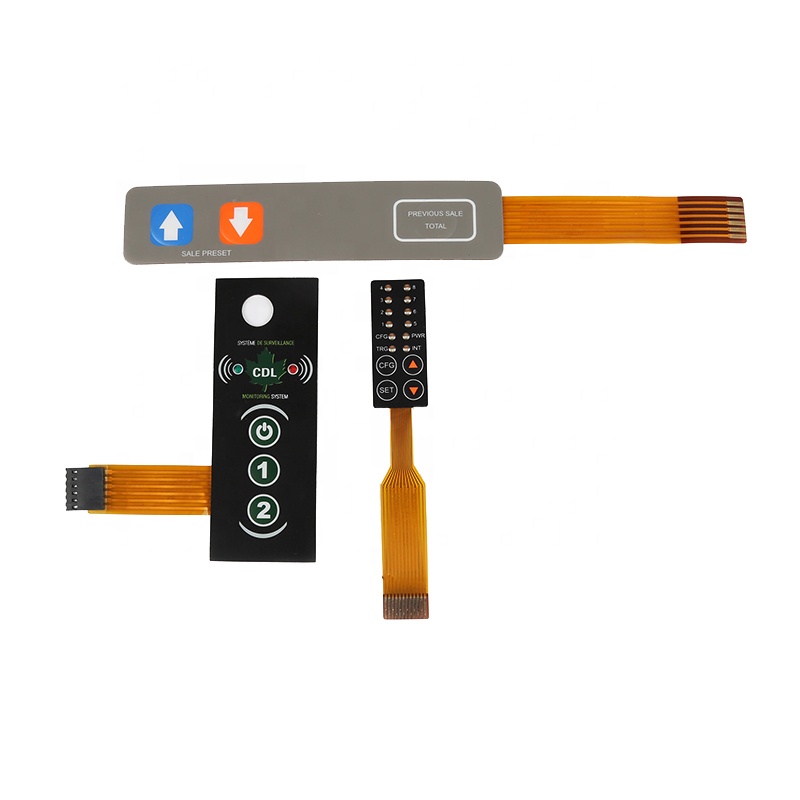
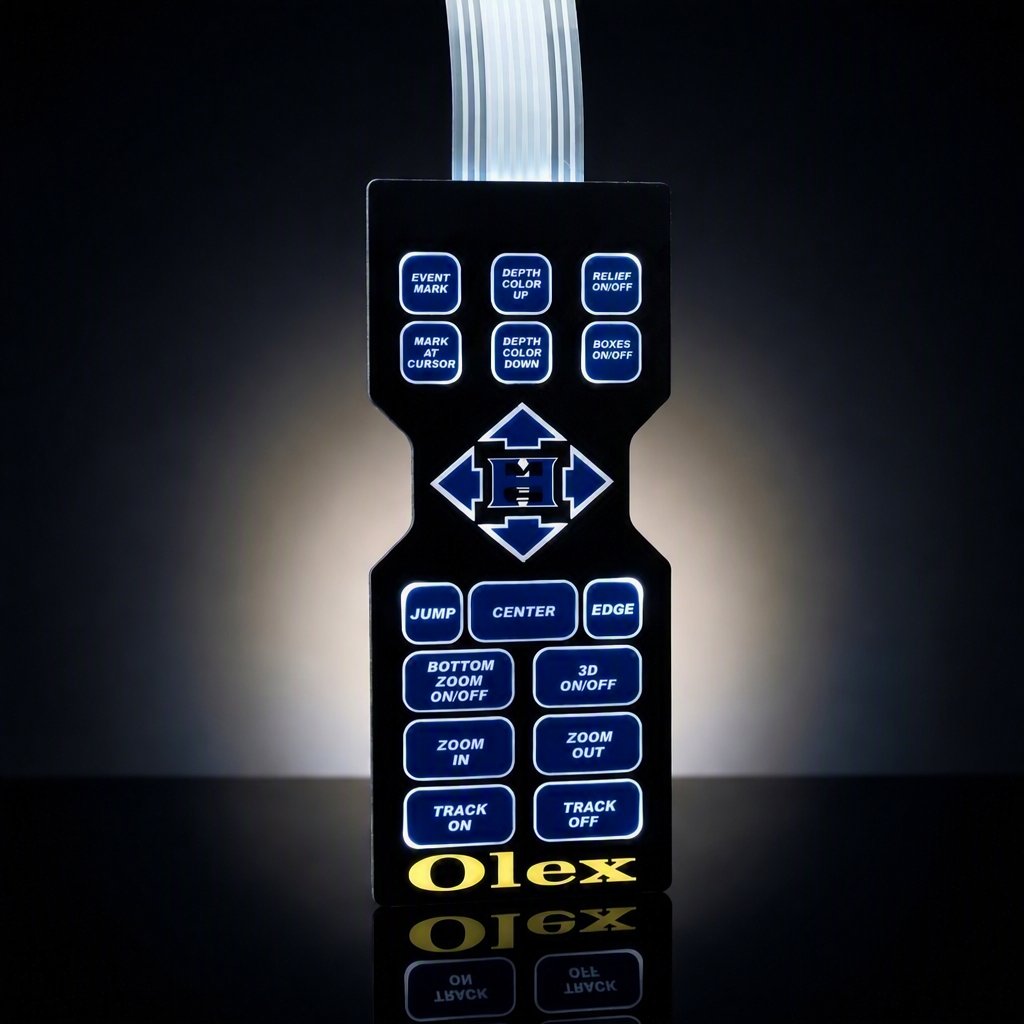
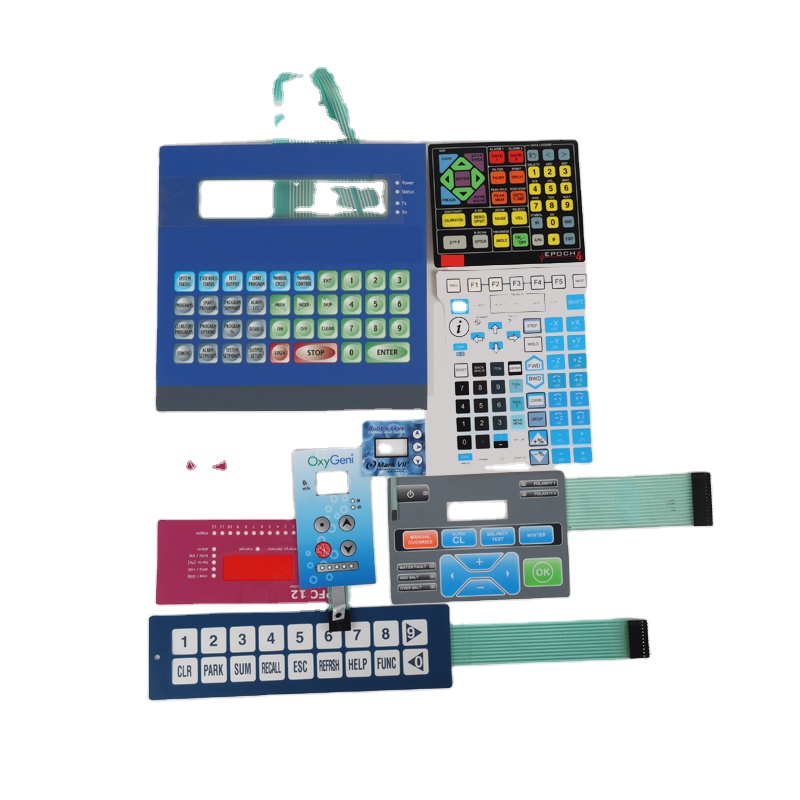
Waterproof Membrane Keyboard Architecture: IP67 & IP68 Sealing Methodology
In demanding industrial environments across Adelaide, South Australia—ranging from beverage bottling plants in the Barossa Valley to naval electronics in Port Adelaide—standard mechanical switches fail prematurely due to liquid ingress, dust accumulation, and chemical corrosion. As a premier China wholesale waterproof membrane keyboard manufacturer, Zhejiang ZIRA Membrane Switch Co., Ltd. builds multi-layer human-machine interfaces specifically engineered to eliminate failure pathways.
Achieving true IP67 or IP68 ingress protection requires a holistic approach to layer stack-up design, adhesive chemistry, and tail outlet sealing. Our engineering team utilizes high-performance graphic overlays, micro-porous venting membranes, and continuous perimeter acrylic gaskets that isolate conductive traces from moisture and caustic atmospheric elements.
Core Structural Layers of a Sealed Waterproof Membrane Switch:
- Graphic Overlay Top Layer: Autotex® EBA/XE textured polyester (PET) or Lexan™ Polycarbonate (PC), featuring chemically resistant matte or gloss finishes, clear display windows, and UV-stabilized inks.
- Top Acrylic Perimeter Seal: Pre-cut high-tack 3M adhesive layer forming an unbroken perimeter barrier around all switch domes and window apertures.
- Tactile Metal Dome Retainer: Precision-placed stainless steel metal domes (four-leg or round, actuation force 220g to 450g) mounted on a dedicated PET dome retainer layer for crisp tactile feedback through heavy work gloves.
- Circuits & Silver/Carbon Conductive Traces: Screen-printed conductive silver paste and protective carbon overcoats on high-flex PET film, or multi-layer FPC (Flexible Printed Circuit) and rigid FR4 PCB boards for high-density SMD LED integration.
- Hydro-Blocking Flexible Tail Exit: Designed with offset internal traces and pot-encapsulated connector junctions, preventing capillary liquid tracking along the ribbon tail into the main enclosure.
- Rear Mounting Adhesive: Heavy-duty 3M VHB or 3M 200MP transfer adhesives formulated to bond permanently to powder-coated steel, stainless steel, cast aluminum, and polycarbonate enclosures.
Localized Application Scenarios across Adelaide & South Australian Sectors
Adelaide has rapidly transformed into a sophisticated hub for high-tech manufacturing, defense innovation, ag-tech, and biomedical development. The operating environments across South Australia demand specialized HMI interfaces tailored to distinct localized operational stressors:
Food, Wine & Beverage Processing (Barossa & McLaren Vale)
Equipment in wine production and food processing undergoes daily high-pressure Clean-in-Place (CIP) washdowns with caustic cleaning agents and hot water. ZIRA’s IP67 sealed PET membrane keyboards resist caustic soda, peracetic acid, and isopropyl alcohol, offering smooth, seamless surfaces that prevent bacterial build-up.
Naval Defense & Maritime Hubs (Osborne Shipyard)
Naval control panels and marine communications deployed along Adelaide’s coast require EMI/RFI shielding to eliminate electronic crosstalk, combined with salt-spray resistance. We incorporate printed graphite/aluminum shielding layers and gold-plated FPC tails tested to withstand 96 hours of salt fog exposure.
Mining & Heavy Machinery (Upper Spencer Gulf & Outback SA)
Extreme airborne iron-dust, ambient heat exceeding 45°C, and intense UV exposure characterize South Australian mining sites. Our UV-resistant Autotex® XE overlays guarantee 1,000+ hours of outdoor QUV weathering protection without yellowing, cracking, or key breakdown under heavy glove actuation.
Medical & BioMed Precinct (Adelaide BioMed City)
Diagnostic tools, patient monitoring systems, and laboratory instrumentation demand sterile, non-porous HMI surfaces. ZIRA manufactures medical-grade PET keypads with antimicrobial surface treatments that withstand continuous hospital-grade disinfectant wipe-downs without legend degradation.
Technical Stack-up Comparison Matrix for Adelaide Buyers
Selecting the optimal membrane keyboard technology requires balancing tactile feel, backlight requirement, IP sealing level, and budget. The matrix below outlines our custom manufacturing options available for Adelaide OEMs:
| Specification Feature | Standard Poly Dome Keypad | Metal Dome Membrane Switch | Capacitive Touch ITO Film | PCB / FPC Rigid Hybrid Keypad |
|---|---|---|---|---|
| Ingress Rating | IP65 - IP67 | IP67 - IP68 | IP68 (Full Flat Glass/PC) | IP67 (Enclosure Sealed) |
| Tactile Feedback | Soft Poly-dome (~180g) | Crisp Snap (220g - 450g) | Zero Travel (Haptic/Audio) | High Crisp Snap (Metal Domes) |
| Actuation Life | > 1,000,000 cycles | > 1,000,000 - 3,000,000 | > 10,000,000 cycles | > 3,000,000 cycles |
| Backlighting Option | Selective Surface LEDs | LED / Light Guide Film (LGF) | Uniform LED Backlighting | High-Density SMT LEDs |
| Chemical / UV Resistance | Good (Standard PET) | Excellent (Autotex PET) | Superior (Glass Overlay) | Excellent (Coated PET Overlay) |
| Target Adelaide Sector | General Electronics | Industrial Washdown / Mining | Smart Home / Clean Medical | Defense / Heavy Automation |
Emerging HMI Trends & Wholesale Direct Sourcing to South Australia
The industrial HMI sector in Australia is undergoing a significant transition toward lighter, more durable, and aesthetically superior control interfaces. Mechanical pushbuttons with physical cutouts are increasingly viewed as legacy failure points due to fluid leaks, contact oxidation, and complex assembly labor.
Key Trends Shaping Adelaide's Keypad Procurement:
1. Integration of Uniform Light Guide Film (LGF): Rather than relying on bulky halogen or incandescent lamps, modern Adelaide OEMs utilize micro-thin LGF layers driven by side-firing SMD LEDs. This delivers whisper-quiet, shadow-free illumination across keys, emergency stop icons, and brand logos while maintaining a profile under 2.0mm thick.
2. Capacitive Touch Overlays with Surface Texture: Combining smooth glass or high-clarity polycarbonate overlays with capacitive ITO (Indium Tin Oxide) film circuits allows touch controls to operate smoothly under glass thicknesses up to 3mm, even when operators wear nitrile or rubber gloves.
3. Direct China Wholesale Factory Sourcing: By eliminating local intermediary distributors in Australia, Adelaide original equipment manufacturers directly access factory-direct pricing, custom prototyping within 5-7 working days, and direct engineering-to-engineering DFM (Design for Manufacturability) support.
Adelaide Procurement FAQs: Custom Membrane Keyboards
Answers to common questions from South Australian design engineers, purchasing managers, and industrial OEMs regarding lead times, shipping, tooling, and quality assurance.
What are the typical shipping times and air/sea freight logistics from China to Adelaide?
For urgent prototype batches and small production runs, we utilize express air freight (DHL, FedEx, UPS) directly to Adelaide Airport (ADL), with transit times averaging 3 to 5 business days. For bulk production orders, sea freight to Port Adelaide typically takes 16 to 22 days. We handle all export documentation, commercial invoices, and tariff HS code classification (e.g., HS 8537.10) for streamlined customs clearance in Australia.
How does ZIRA ensure waterproof integrity (IP67/IP68) on custom keyboard orders?
Every waterproof membrane switch order undergoes rigorous in-house testing. We utilize custom pneumatic pressure-decay testing fixtures to verify perimeter adhesive sealing. Furthermore, sample switches from each production batch undergo immersion testing (IP67: 1 meter depth for 30 minutes; IP68: custom depth/duration) and thermal cycling (-40°C to +85°C) to ensure zero delamination or moisture ingress occurs in field conditions.
What graphic drawing formats do you accept for custom OEM/ODM tooling?
Our engineering department works directly with standard CAD vector and artwork files, including AutoCAD (.DXF, .DWG), Adobe Illustrator (.AI), vector PDF, SolidWorks (.STEP, .IGES), and CorelDraw. If you only have a physical sample or hand sketch from an existing control panel, our engineering team provides full reverse-engineering and DFM layout services free of charge.
What is your Minimum Order Quantity (MOQ) for Adelaide businesses?
We support both low-volume high-mix prototypes and mass production. Prototype samples can be ordered starting at 1 to 5 pieces for initial engineering evaluation. Standard production runs typically start at 100 pieces. For standardized numeric PET keypads, wholesale tier pricing applies at 1,000+ units.
Are ZIRA's membrane keyboards compliant with Australian and International environmental standards?
Yes. All materials utilized—including PET films, PC sheets, silver pastes, stainless steel domes, and 3M adhesive backings—are strictly compliant with RoHS 3.0, REACH, and WEEE directives. Certification documents and material safety data sheets (MSDS) are supplied with every shipment to support your compliance audits under Australian Standards (AS/NZS).
Why Partner with Zhejiang ZIRA Membrane Switch Co., Ltd.
Combining 29+ years of manufacturing expertise with rigorous quality assurance systems to deliver defect-free human-machine interface solutions worldwide.
Established Manufacturing Heritage (1996)
Over nearly three decades, ZIRA has evolved into an industry leader, operating 5,000 m² of specialized production floor space in Changhe Industrial Park, Ningbo, featuring dust-free cleanrooms for printing and lamination.
Intertek Onsite Verified Supplier
Our production facilities, testing capabilities, legal status, and QA/QC procedures have been verified onsite by Intertek. We maintain ISO 9001:2015 certified quality management systems.
100% Electrical & Visual QC Inspection
Zero-defect commitment: Every finished switch panel undergoes automated 100% circuit continuity testing, contact resistance measurement, loop resistance check, LED polarity verification, and meticulous visual inspection prior to export packing.
Trusted Partner to Global Fortune 500s
We maintain long-term supply relationships with global industrial automation giants such as ABB and Emerson, providing custom keypads that satisfy strict international electrical and durability standards.
Request Your Custom Keypad Quote for Adelaide Projects
Send your dimensional drawings, circuit schematics, or color specifications to our engineering team today. Get rapid DFM feedback, stack-up recommendations, and direct wholesale pricing within 24 hours.
