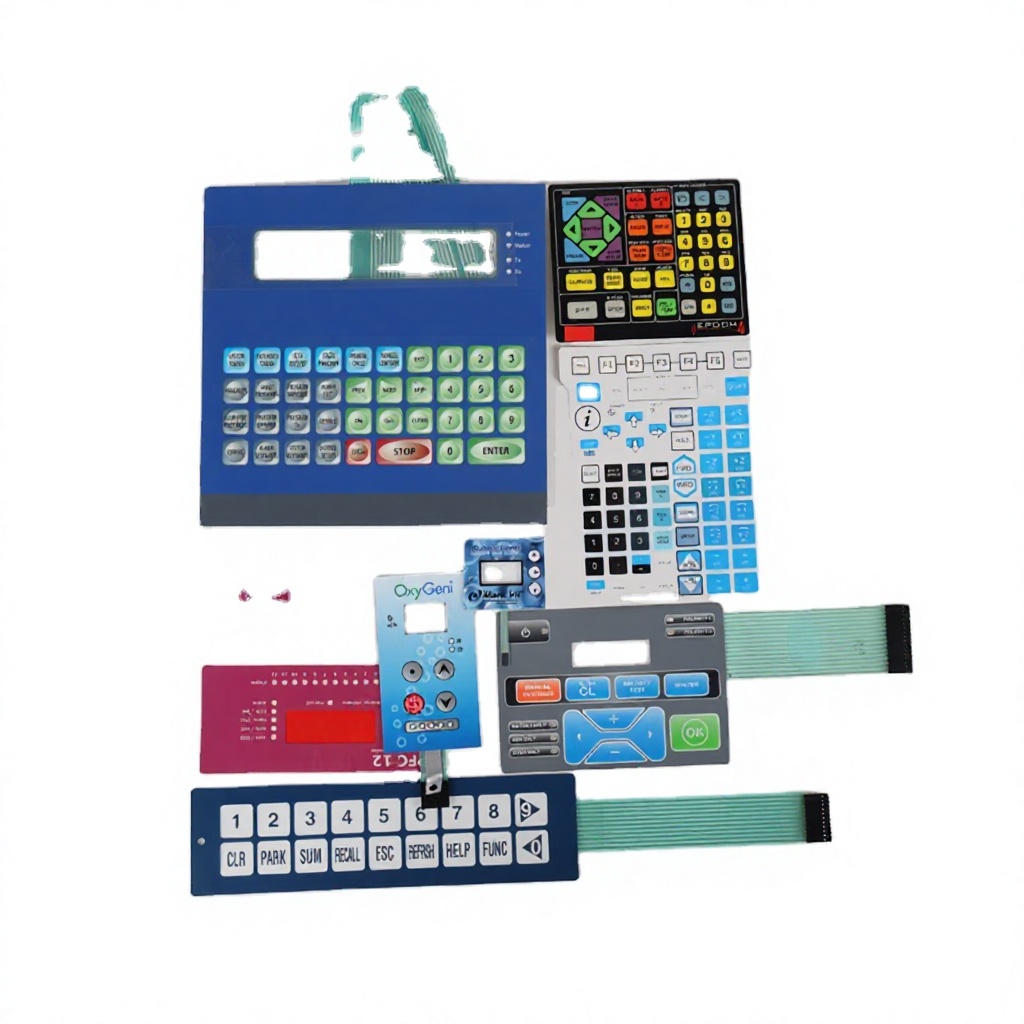
RoHS REACH Compliant UL94V0 IP67 Tactile Membrane Keyboard
IP67 perimeter watertight seal, flame-retardant circuit, pristine tactile snap ratio for field instruments.
Get Catalog
Explore our certified sealed membrane panels, industrial push-buttons, and ESD-shielded input systems customized to exact dimensional and electrical schematics.
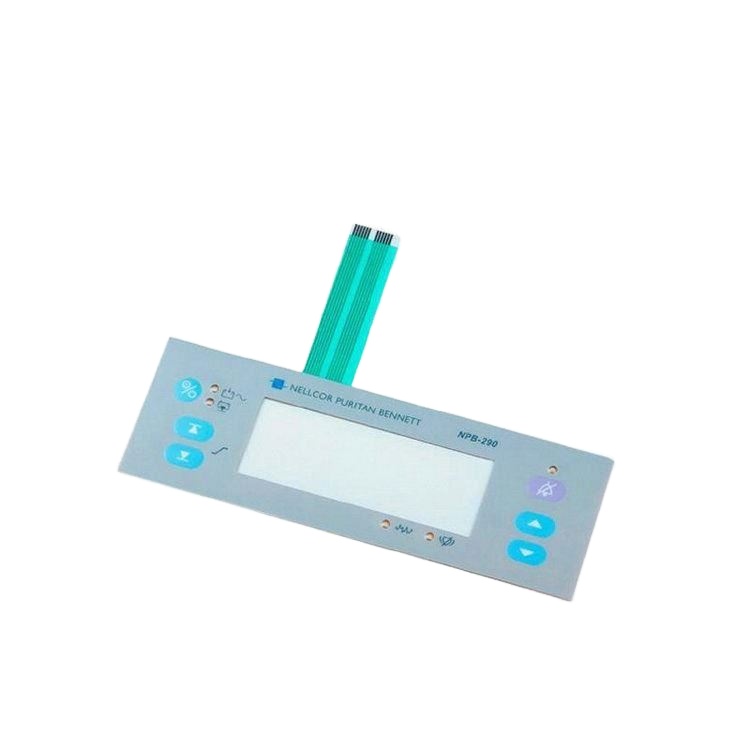
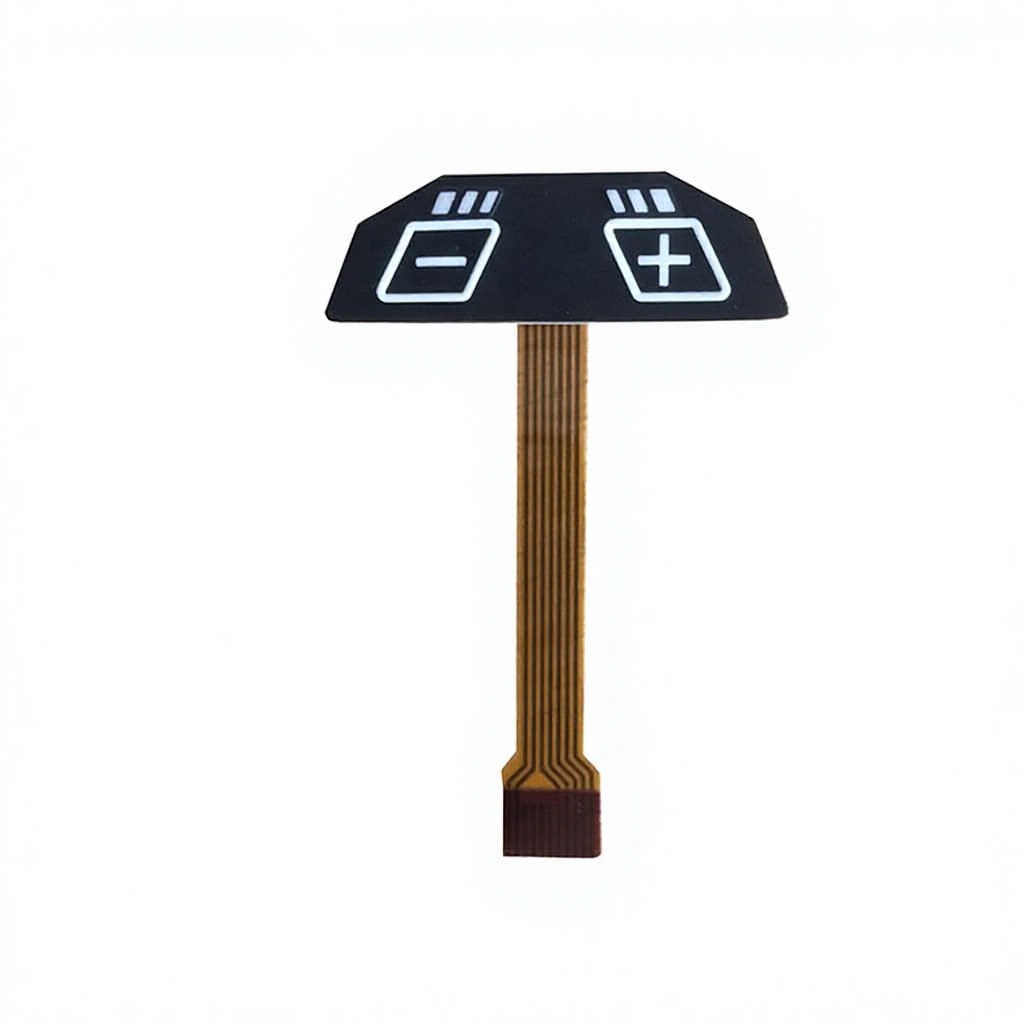
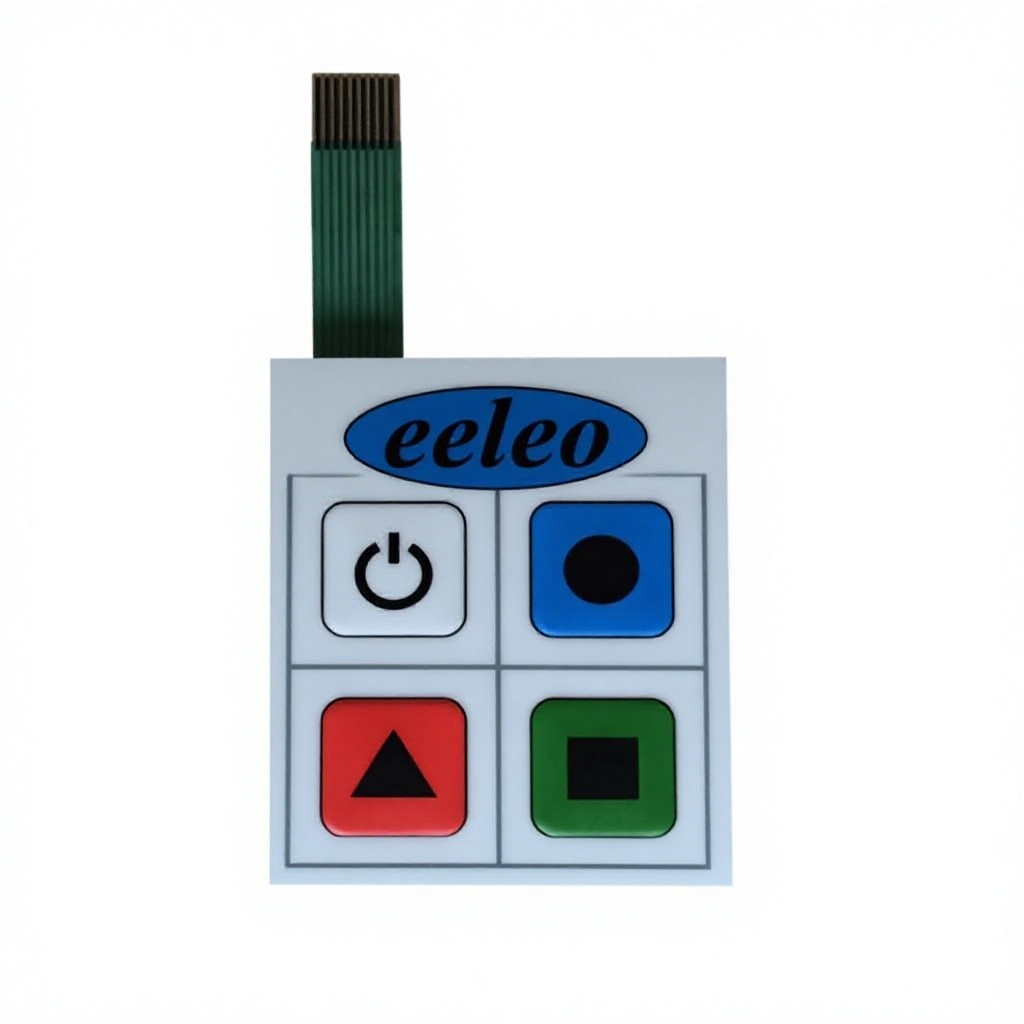
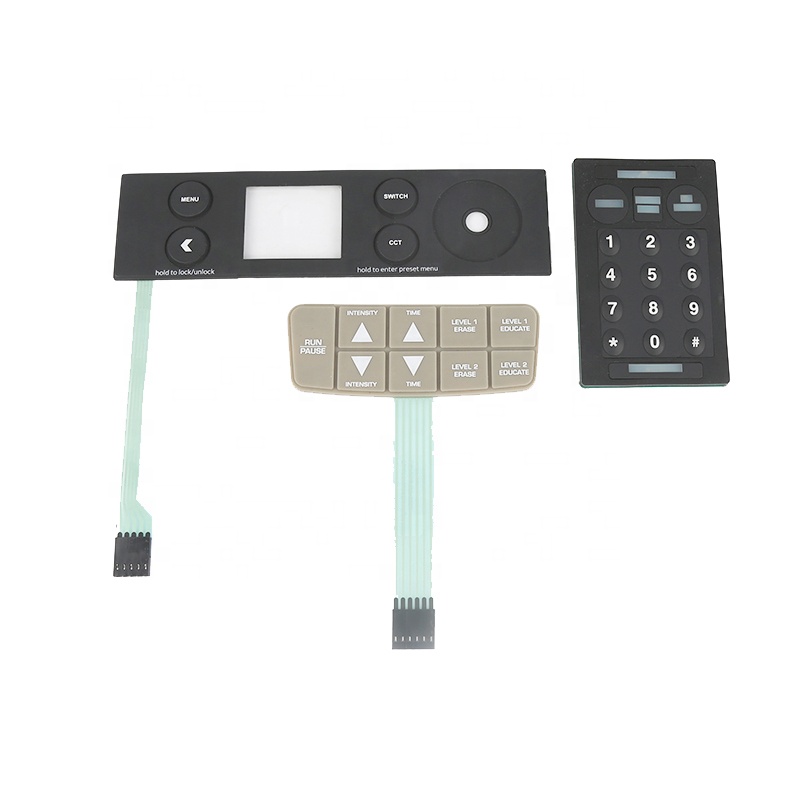
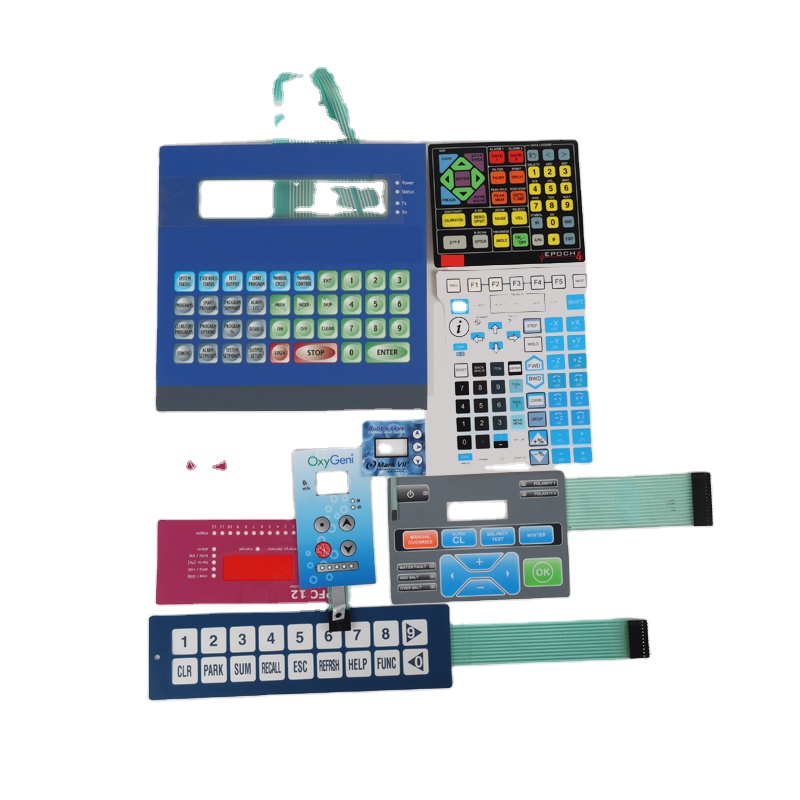
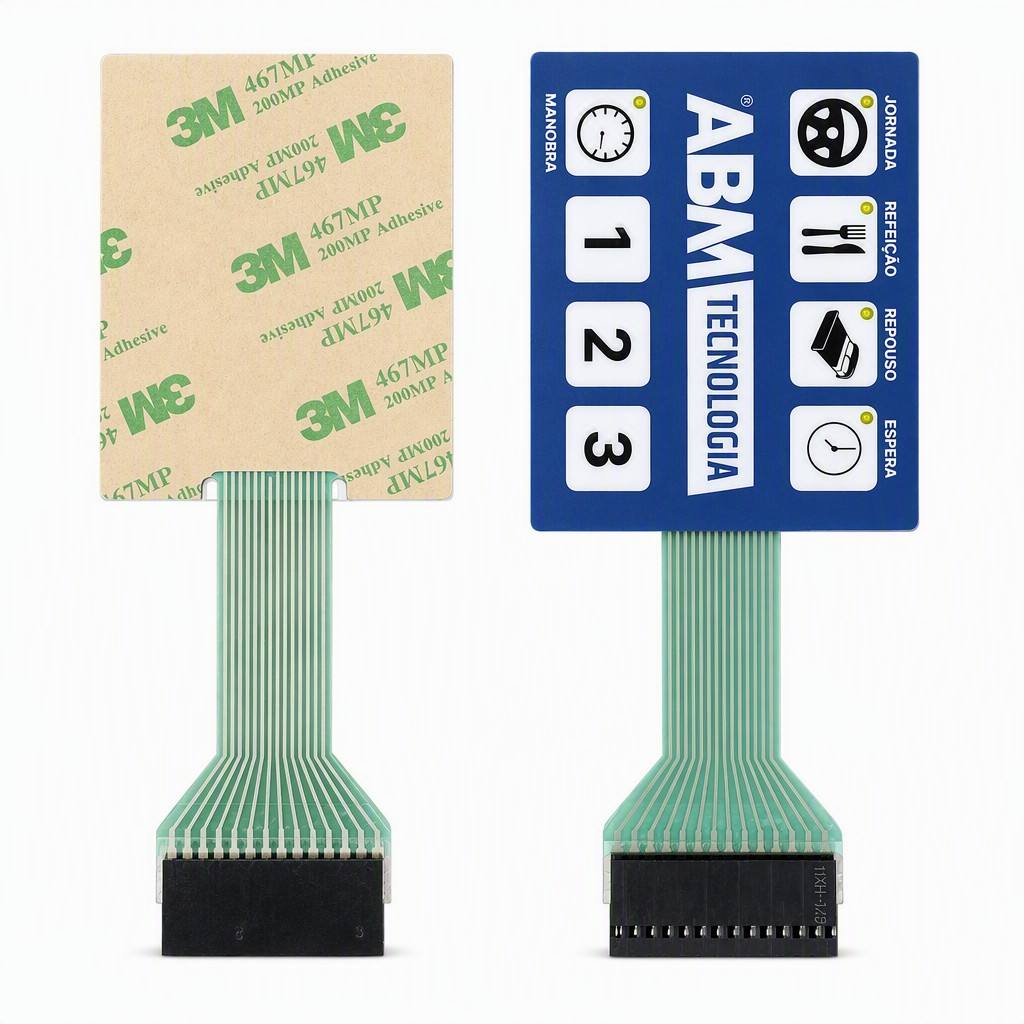
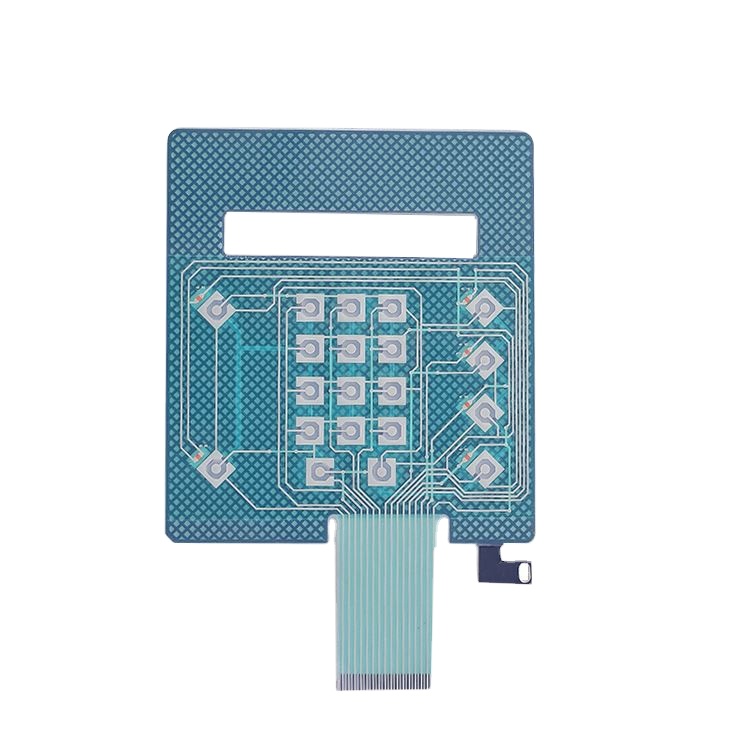
A comprehensive examination of environmental durability, compliance standards, and supply chain synergy for OEMs operating across the Cumberland Valley.
The Greater Nashville metropolitan area, extending through Davidson, Rutherford, Williamson, and Wilson counties, has evolved far beyond its classical trade origins into a high-technology industrial, automotive assembly, and healthcare innovation center. For original equipment manufacturers (OEMs) operating within Middle Tennessee, selecting human-machine interface (HMI) hardware requires addressing tough operational challenges: sudden humidity fluctuations, airborne chemical cleaners, grease exposure in automotive subsystems, and rigorous sanitation cycles in surgical and analytical suites.
As an established export-oriented factory with nearly three decades of dedicated production experience, Zhejiang ZIRA Membrane Switch Co., Ltd. provides Nashville engineering teams direct factory access to custom-engineered, fully sealed membrane switches, flexible printed circuits (FPC), tactile silicone overlays, and integrated backlighting systems. By bridging direct component manufacturing with rigorous international compliance (ISO 9001:2015, RoHS, REACH, UL94V-0), we ensure that procurement teams and system architects in Middle Tennessee eliminate middle-tier distributor markups while securing aerospace-grade assembly consistency.
Serving Nashville's expansive healthcare systems and diagnostic instrument developers. Our keypads feature medical-grade Autotex PET overlays resistant to harsh hospital disinfectants, quaternary ammonium compounds, and isopropyl alcohol wipes, achieving fluid-tight IP67 ratings for sterilization protocols.
With Middle Tennessee being a premier automotive production hub, our tactile assemblies meet stringent thermal cycling (-40°C to +85°C), high vibration resistance, and custom EMI/RFI shielding configurations required by Tier-1 transportation and logistics robotics suppliers.
Machinery deployed throughout Tennessee's diverse processing plants encounters airborne debris, lubricants, and high mechanical shock. We deploy deep-drawn tactile metal domes with tactile snap ratios over 50% and 3M 300LSE adhesive bonds designed for low surface energy plastics and powder-coated cast metals.
Achieving true environmental isolation demands exact cohesion across the multi-layer membrane switch stack-up. The diagrammatic layout of an industrial-grade sealed membrane switch relies on selective sub-surface screen printing, precision-vented spacer layers, and airtight perimeter seals. Below is the standard engineering breakdown employed by ZIRA for Nashville procurement specifications:
| Layer Sequence | Material Specification | Functional Contribution to Durability | Inspection Standard |
|---|---|---|---|
| 1. Graphic Overlay | Autotex XE / F150 / F200 Textured PET | Chemical resistance against oil, ketones, bleach; UV-blocking outdoor durability. | ASTM D3363 (Pencil Hardness 3H), Gloss meter check |
| 2. Overlay Adhesive | 3M 467MP / 200MP High-Performance Acrylic | Airtight bond between overlay and upper circuit layer, preventing liquid ingress. | Peel adhesion test (>20 N/100mm), Zero bubbling audit |
| 3. Upper Circuit Layer | Heat-stabilized PET + Conductive Silver / Carbon Ink | Carries upper contact traces; low sheet resistance (<0.05 Ω/sq/mil). | Automated trace conductivity & continuity testing |
| 4. Circuit Spacer | Optically clear polyester with double acrylic adhesive | Internal venting channels equalizing barometric shifts without breaching IP67 seals. | Die-cut dimensional tolerance within ±0.05 mm |
| 5. Lower Circuit / Metal Domes | Stainless Steel Nickel-Plated / Gold-Plated Domes | Provides tactile actuation snap feedback (250g–500g force); >5 million clicks. | Dynamic life cycling test, contact bounce <5ms |
| 6. Rear Mounting Adhesive | 3M 468MP or 300LSE for Textured/LSE Casings | Binds finished switch assembly to metal chassis or plastic instrument housing. | Shear strength validation, ASTM D3330 compliance |
Through our dedicated design-for-manufacturability (DFM) review protocol, our engineers scrutinize track routing, tail trace bend radii, and anti-static ESD cages before tooling begins. This attention to detail eliminates silver migration issues caused by humidity in high-temperature environments, ensuring your equipment functions reliably in both climate-controlled laboratories and unconditioned industrial facilities.
A direct partnership offering complete technical autonomy, fully auditable QA workflows, and competitive factory-floor economics.
Our manufacturing complex in Ningbo is independently audited and verified onsite by Intertek. We maintain structured QA/QC protocols across raw material intake, screen tensioning, cleanroom silver printing, and thermal oven sintering, offering full lot traceability for overseas clients.
Whether you require a rapid 5-piece functional prototype for local pilot testing in Tennessee or high-volume recurring monthly production of 100,000 units, our scalable production lines adapt cleanly to your supply schedule without compromising tolerances.
100% of manufactured units undergo comprehensive electrical verification, loop resistance confirmation, insulation checks (>100MΩ at 100V DC), visual surface inspection, and tactile snap validation before air cargo or sea freight dispatch.
Direct answers addressing technical trade, testing, shipping timelines, and custom switch engineering.
Consult directly with our senior HMI design engineers. Receive comprehensive DFM reviews, accurate material costings, and complete technical documentation tailored for your Nashville project.
Get Catalog