High-Reliability Backlit Keypads & Membrane Interface Solutions
Engineered to withstand rigorous operational cycles, UV exposure, and stringent industrial sanitation. Explore our direct factory-manufactured product series specified by engineering procurement managers across Victoria, Australia.
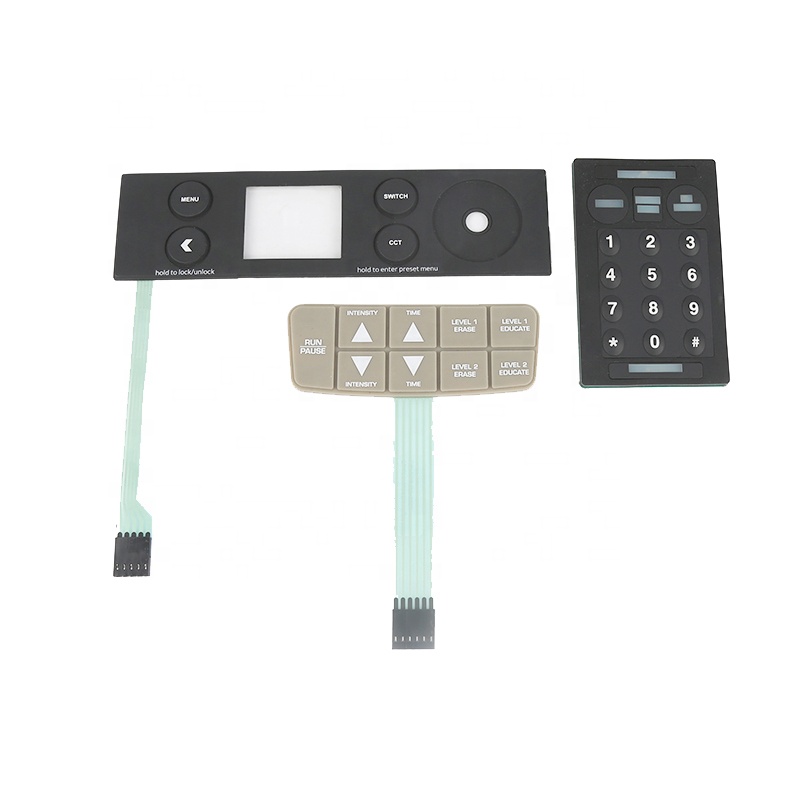
Customize High Sensitivity Metal Dome 3M Adhesive Medical Membrane Switch
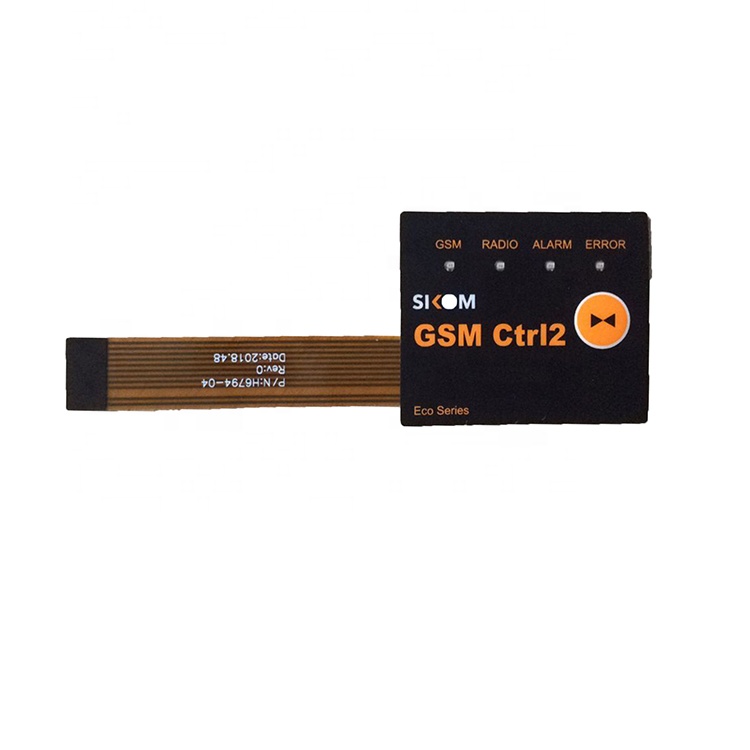
RoHS Compliant Industrial Membrane Push Button Switch for Medical Control Panels
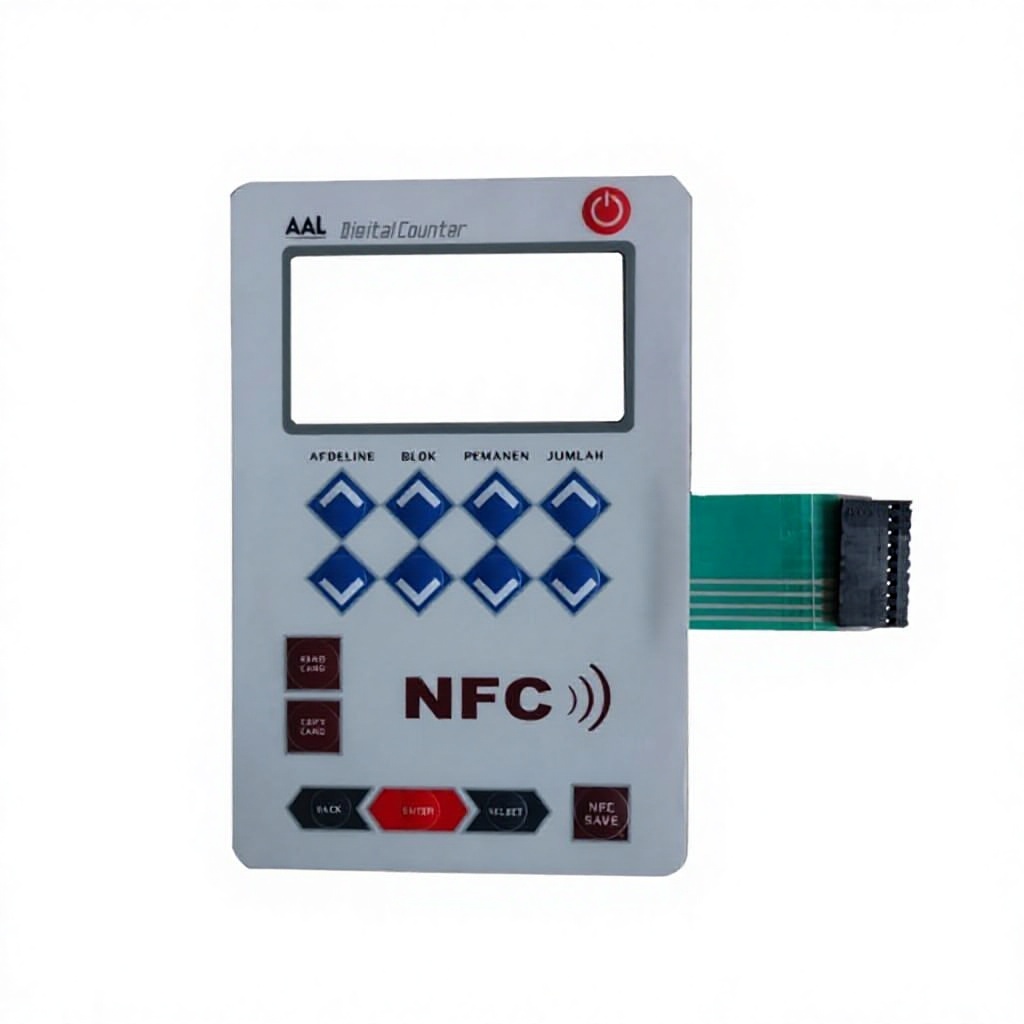
Polyester Dome or Metal Dome Options Rated 1 Million Instrumentation Keypad
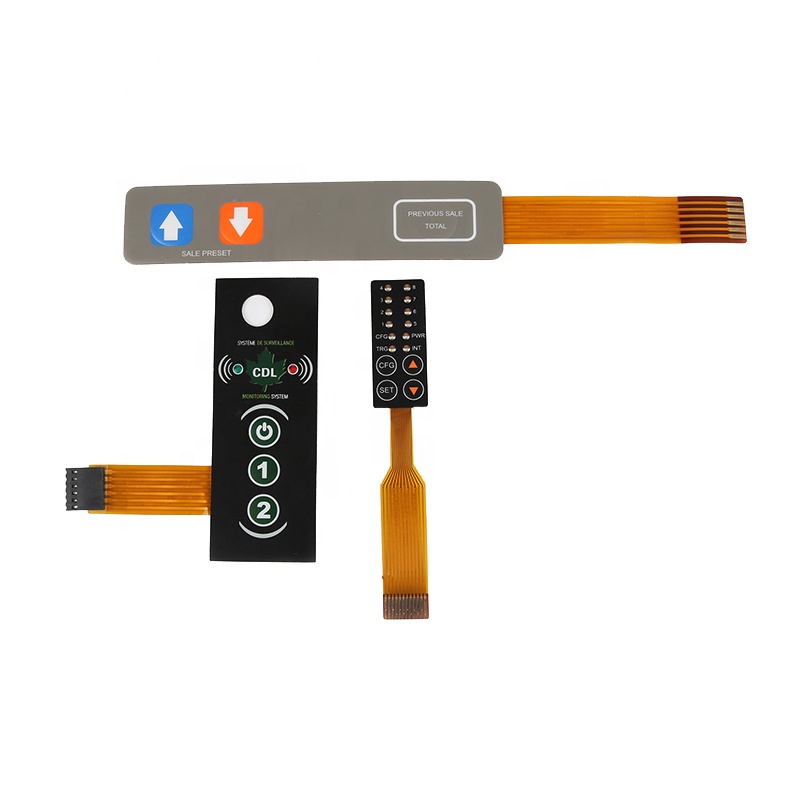
High-Performance OEM Membrane Key Switch with LED Backlight for Control Panels
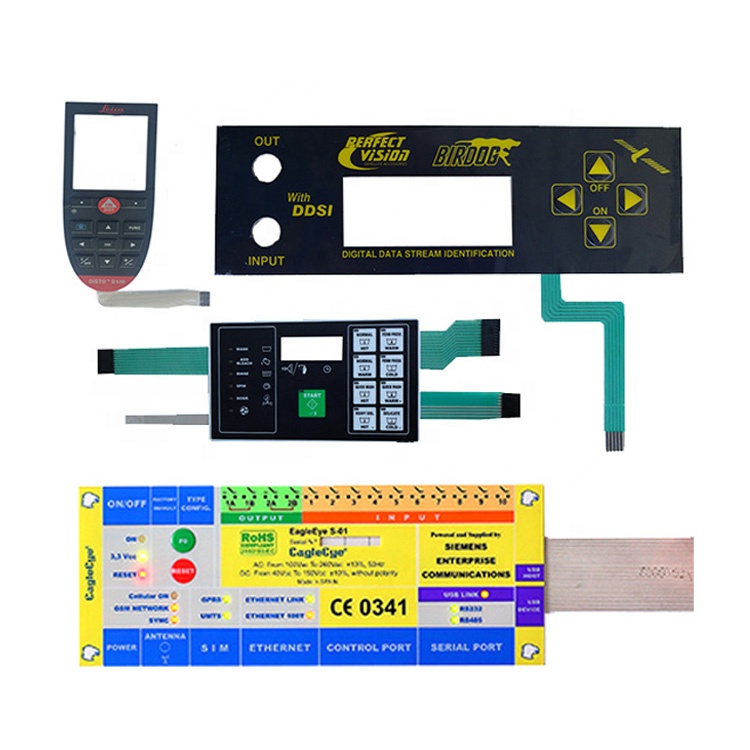
Waterproof Industrial Membrane Panel with Shock Resistance Feature

Waterproof Capacitive Touch Membrane Switch Customizable Color & Texture
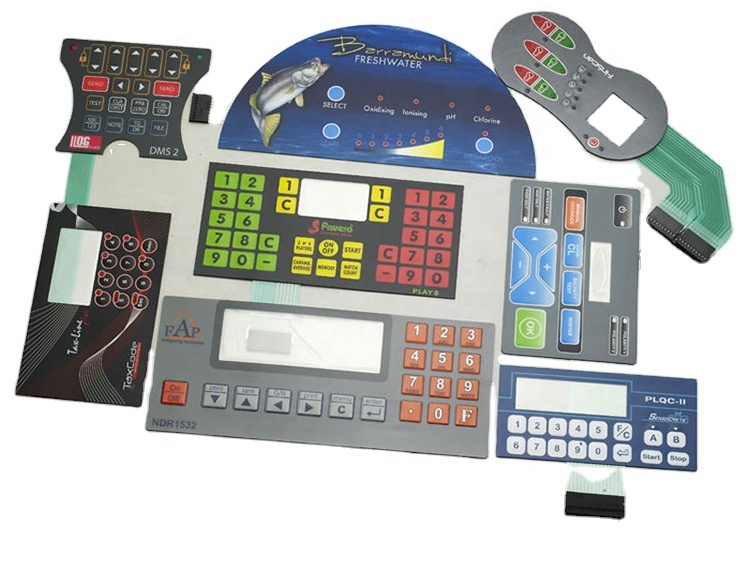
Custom Membrane Keyboards LED Backlit Membrane Switch for Quick Sampling
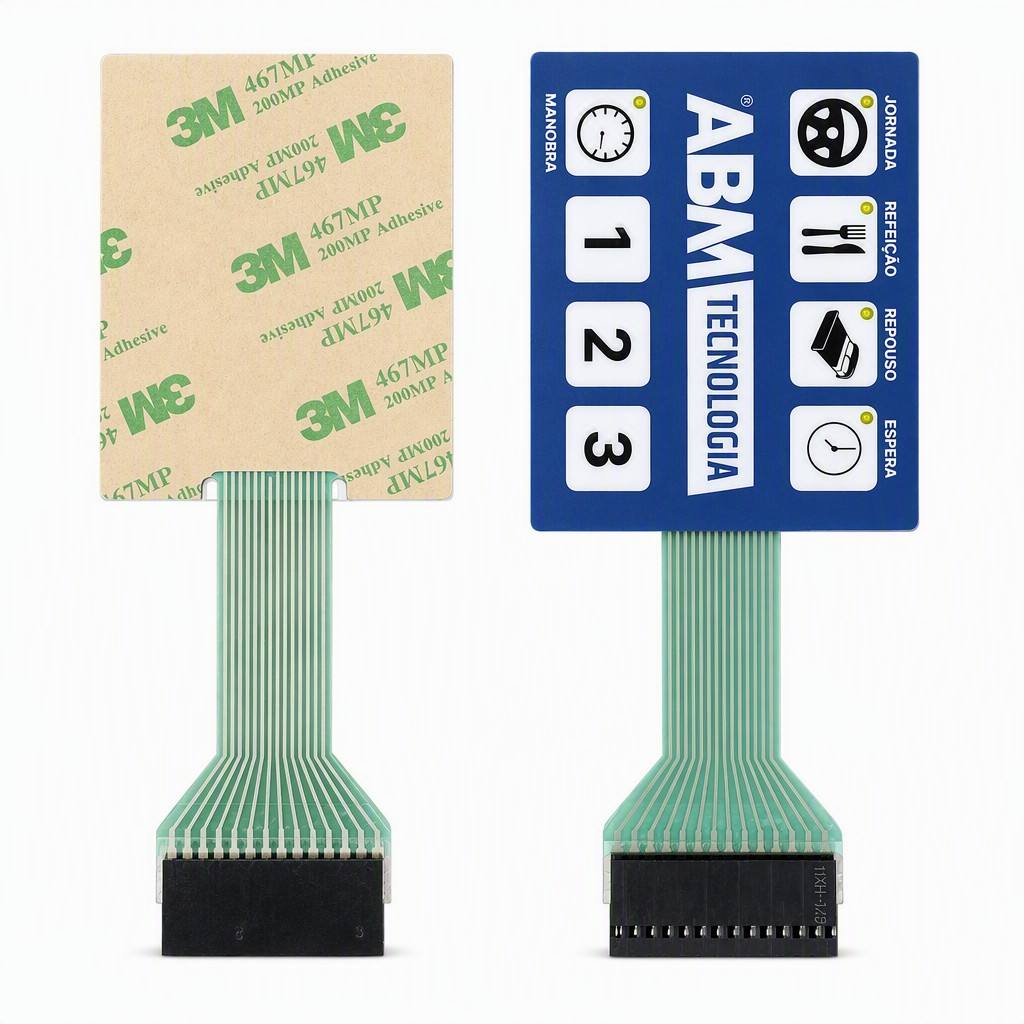
Custom Membrane Switch Industrial Control Panel Keypad Tactile Metal Dome
Specialized HMI Deployments Across Victoria’s Key Industrial Corridors
Victoria's transition into advanced automation, medical technology commercialization, and renewable energy infrastructure demands front-panel interfaces capable of enduring harsh environmental and clinical stress. Zhejiang ZIRA delivers custom illuminated keypads tailored to local operational standards.
Melbourne Biomedical & MedTech Precinct
Centred around Parkville and Clayton, Victoria leads the southern hemisphere in clinical device design. Our backlit membrane switches support medical centrifuges, patient monitors, and point-of-care diagnostics requiring antimicrobial Autotex PET, sealed IP67 wipe-down surfaces, and low-glare LED backlighting for nocturnal ICU operation.
- Hospital disinfectant & IPA resistance
- Continuous anti-microbial textured overlay
- AS ISO 13485 manufacturing compliance
Latrobe Valley Heavy Industry & Clean Energy
As the Latrobe Valley transitions from coal generation toward hydrogen, biomass, and microgrid infrastructure, control cabinets must resist extreme airborne particulates, chemical vapours, and solar thermal cycling. Our heavy-duty tactile keypads utilize 3M 300LSE adhesive matrices and metal domes to withstand abrasive field handling.
- IP68 gas-tight perimeter barrier seals
- Operating range: -40°C to +85°C
- High-tactile snap feedback with gloved hands
Geelong & Dandenong Advanced Manufacturing
Victoria's automotive legacy has transformed into precision transport engineering, aerospace composites (Fishermans Bend), and automated packaging lines in Dandenong and Geelong. Our integrated PCB/FPC-backed membrane switches provide direct connector termination to PLC backplanes with integrated surface-mount status LEDs.
- Direct FR4 or polyimide FPC rigid-flex boards
- Tested over 5,000,000 actuation cycles
- Vibration tested to MIL-STD-202G specs
Goulburn Valley AgTech & Marine Coastal
Across regional Victoria (Shepparton dairy, Sunraysia citrus automation) and coastal maritime fleets (Port Phillip Bay, Westernport), electronics face destructive UV indices and high saline humidity. We laminate with specialized UV-inhibited Autotype XE films and silicone seal gaskets that block moisture-induced silver dendrite migration.
- UV exposure rating > 1,000 hrs ASTM G154
- Salt fog corrosion resistant (ASTM B117)
- NEMA 4X / IP67 outdoor washdown rated
Comparative Analysis of Backlighting Architectures in Modern HMIs
Illumination integrity is paramount for industrial safety, user experience, and low-power efficiency. Design engineers evaluating backlighting options must balance stack-up thickness, thermal dissipation, mechanical travel, and luminance uniformity.
In standard membrane keyboards, illumination has historically relied on surface-mount (SMT) LEDs embedded inside spacer cutouts. While effective for localized point indicators, achieving homogenous illumination across large legends or full key matrices requires advanced optical design. The integration of Light Guide Film (LGF) technology has disrupted traditional front-panel engineering. LGF uses ultra-thin (0.125mm to 0.25mm) precision-molded polycarbonate or optical-grade acrylic films micro-etched with light-extracting dot matrix arrays. By directing side-firing SMT LEDs laterally across the film, light is redirected vertically toward the user, producing exceptional uniformity (>90%) with zero hot-spotting and negligible power draw.
| Evaluation Parameter | Light Guide Film (LGF) Membrane | Discrete Surface-Mount (SMT) LEDs | Electroluminescent (EL) Foil | Silicone Light-Pipe Keymat |
|---|---|---|---|---|
| Typical Stack-up Thickness | 0.8 mm – 1.4 mm Ultra-Thin | 1.2 mm – 2.2 mm | 0.6 mm – 1.0 mm | 3.5 mm – 8.0 mm (Full Travel) |
| Luminance Uniformity | Exceptional (85% – 95% uniform) | Localized hot-spotting (indicators only) | 100% perfectly homogenous | Moderate to high via laser etching |
| Operating Voltage & Power | 3.0V – 5.0V DC (Standard bus) | 2.0V – 3.3V DC per LED | 60V – 120V AC (Requires Inverter) | 3.0V – 5.0V DC bus |
| Half-Life Degradation | 50,000+ Operating Hours | 50,000+ Operating Hours | 3,000 – 6,000 Operating Hours | 50,000+ Operating Hours |
| Tactile Feedback Integration | Full tactile with stainless domes | Full tactile dome integration | Soft feel or non-tactile switch | Deep elastomer stroke (1.5mm–2.5mm) |
| Ingress & Environmental Seal | IP65 – IP68 hermetic sealing | IP65 – IP67 sealing | Moisture sensitive; edges prone to seal leak | Perimeter compression gasket fit |
| Victorian Industry Best-Fit | MedTech consoles & handheld diagnostics | Industrial machinery status panels | Specialized aerospace / darkroom | Mining handhelds & tele-remote units |
Why Australian OEMs Partner with Zhejiang ZIRA
Direct sourcing from a verified primary manufacturer eliminates redundant trading tier markups, streamlines engineering communication, and guarantees end-to-end accountability under one roof in Ningbo, Zhejiang.
Third-Party Certified Integrity
Our 5,000m² manufacturing facility is verified onsite by Intertek. Comprehensive supplier assessment audits cover quality management systems (ISO 9001:2015), legal standing, workforce safety, and trace testing records, giving Australian procurement committees verifiable confidence.
Cleanroom Screen Printing
Optical window transparency and precision conductive silver circuitry require an aerosol-free environment. We perform layer deposition and ultraviolet curing in temperature-controlled Class 1,000 and Class 10,000 cleanrooms, eliminating pinhole voids and cosmetic particulates.
Trusted by Industrial Leaders
For more than two decades, Zhejiang ZIRA has maintained active supply relationships with multinational automation giants including ABB and Emerson. Our engineering department understands strict corporate DFM protocols, drawing revision controls, and PPAP documentation.
100% Automated Electrical Check
Every single manufactured keypad undergoes automated electrical continuity verification, loop resistance testing, LED polarity and forward-voltage validation, and insulation dielectric breakdown analysis before packaging. No untested batch ever leaves our facility.
Frequently Asked Questions by Victorian Purchasing Teams
Clear, definitive engineering and commercial answers regarding lead times, Australian import regulations, ChAFTA preferential duties, tooling expenditures, and environmental compliance.
What customs tariffs apply when importing membrane keypads from China into Victoria, Australia?
What are the transit lead times from your Ningbo factory to Melbourne, Victoria?
How do you ensure switches comply with Australian environmental and safety standards?
What technical documentation is required to receive an engineering DFM and quotation?
- Mechanical & Graphic Artwork: Vector files (.DXF, .DWG, .STEP, .AI, or .PDF) detailing dimensions, key shapes, window transparent/translucent zones, and embossing profiles.
- Color Specifications: Pantone (PMS) or RAL colour codes for precise ink matching.
- Circuit Schematic: Common bus, matrix pinout, or tail pin connection assignment, including tail pitch (1.0mm, 1.27mm, or 2.54mm) and connector housing brand (FCI, Nicomatic, or ZIF bare tail).
- Operating Environment: Required tactile force (typically 250g to 450g), operating temperature parameters, backlighting luminance requirements, and IP sealing class.
Can we procure small batch pilot runs for Australian clinical trials or R&D validation?
How does Zhejiang ZIRA prevent silver migration in humid or coastal Victorian regions?
Accelerate Your Victorian HMI Project with Factory-Direct Engineering
Send your CAD drawings, graphic overlays, or functional schematics today. Our Ningbo-based engineering team will deliver a comprehensive Design-for-Manufacturability (DFM) review, material stack-up proposal, and transparent factory-direct pricing within 24 hours.
