Industrial & Medical Grade Plastic Keypad Assemblies
Engineered for extreme operating environments. Our CE-compliant plastic keypad assemblies, tactile membrane matrices, and backlit silicone elastomeric interfaces deliver uninterrupted mechanical integrity under continuous maritime humidity, thermal stress, and chemical contact.
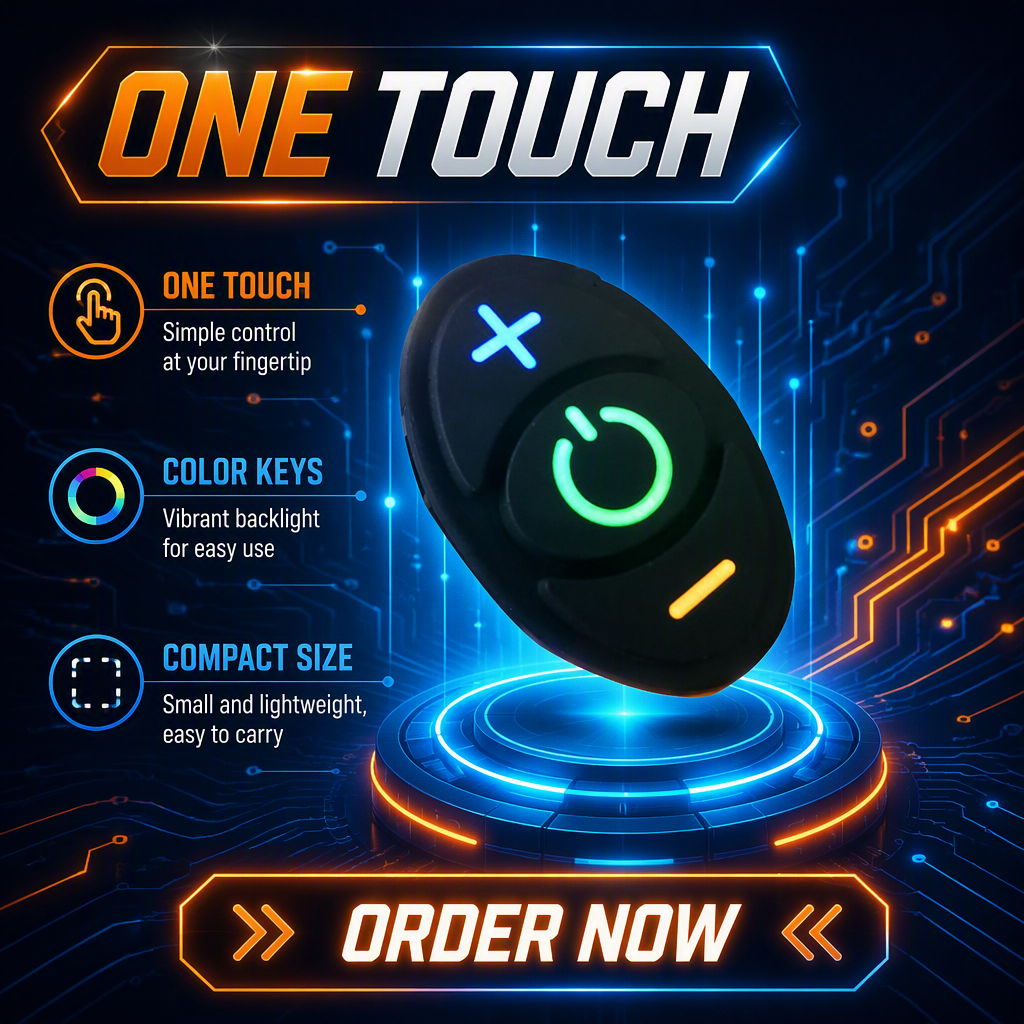
Multi-Zone Backlit Silicone Rubber Membrane Switch
Independent circuit routing with zero light bleed. Precision-molded translucent silicone elastomer integrated with tactile domes.
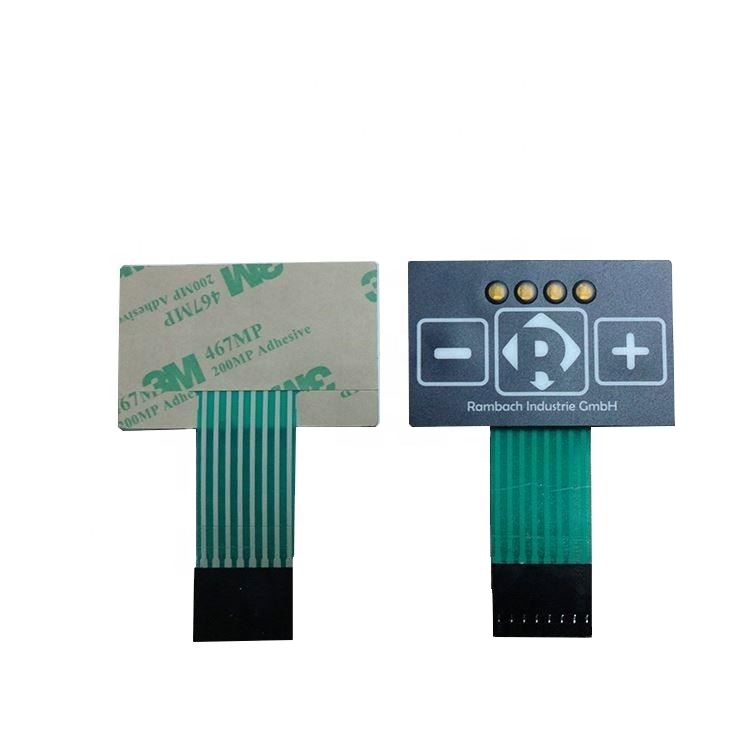
Custom Thin Film Illuminated Panel LGF/LED Switch
Ultra-thin Light Guide Film (LGF) architecture providing uniform surface luminance at low electrical power consumption for solar installations.
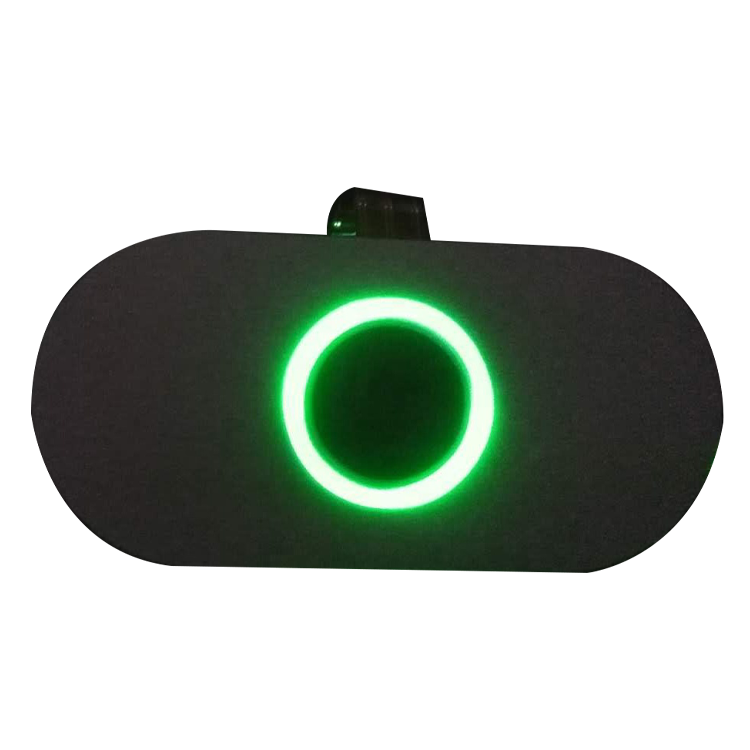
Industrial LED Backlit Tactile Metal Dome Keypad
High-reliability gold and nickel-plated stainless steel metal domes providing crisp tactile snap ratio and extended 1,000,000+ actuation lifecycle.
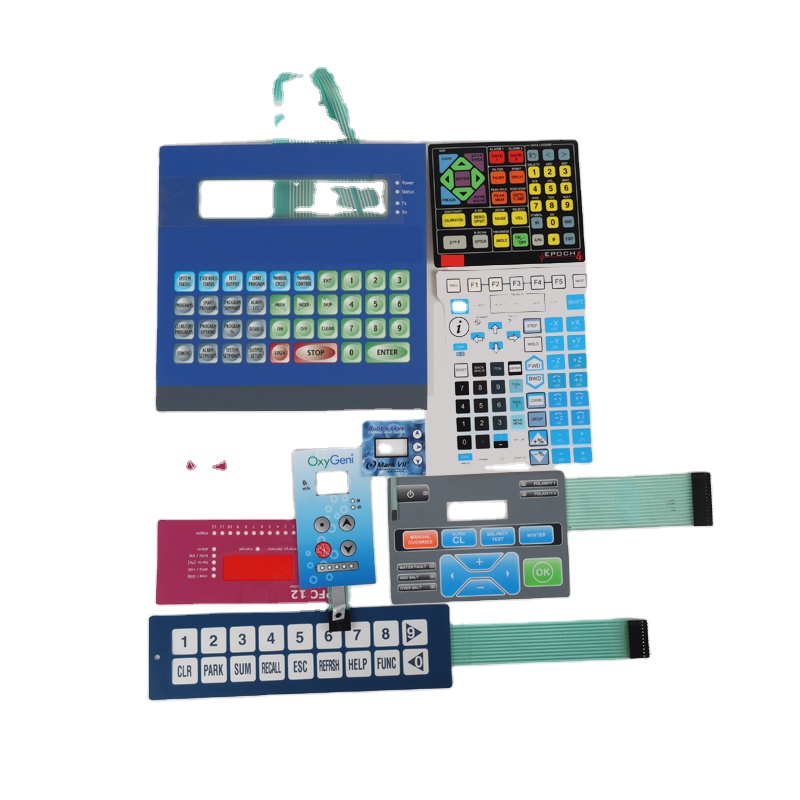
Medical Grade PET Keypad with 3M Adhesive Backing
Antimicrobial surface treatment with high resistance to hospital-grade disinfectants, alcohol wiping, and continuous saline aerosol contact.
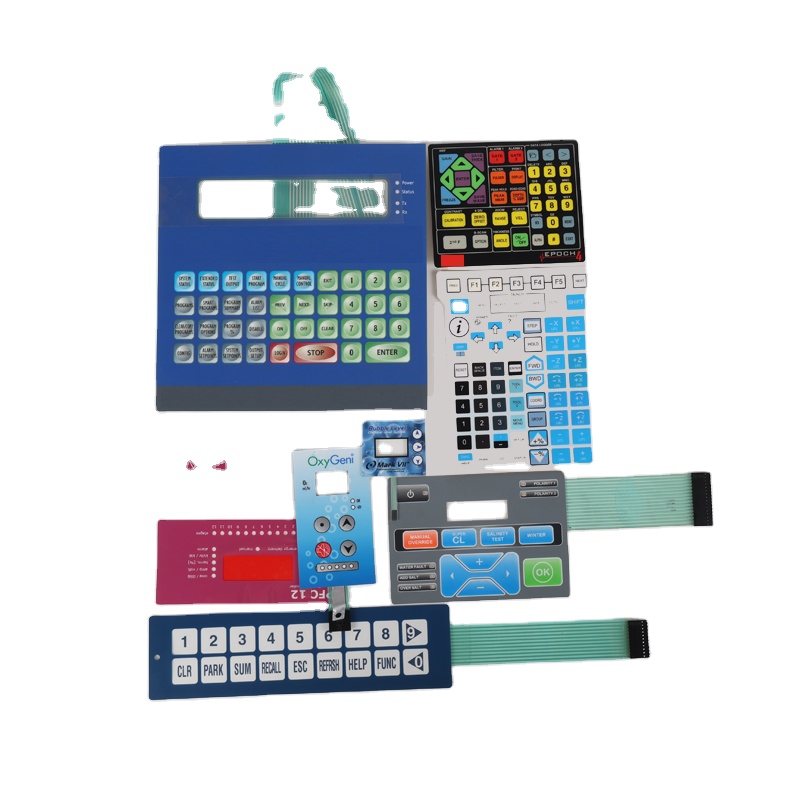
Waterproof Flexible Circuit Membrane Switch Panel
Hermetically enclosed internal silver printed traces shielded by carbon overcoat layers preventing moisture ingress and galvanic silver electromigration.
IP67 Tactile Membrane Keyboard (UL94-V0 Optional)
Flame retardant substrate options complying with UL94-V0 flammability standards, verified for offshore utility housings and critical controls.
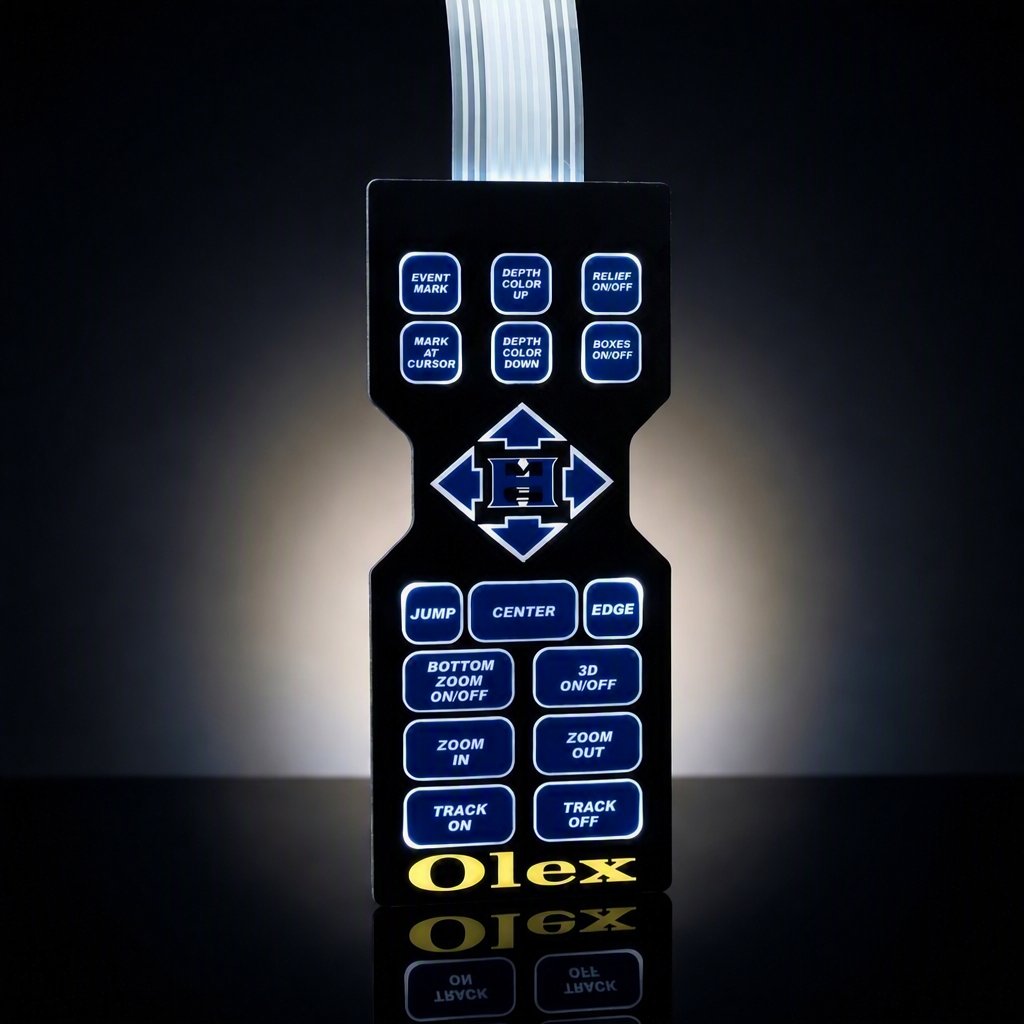
Uniform Illumination Backlight Membrane Keyboard
Engineered with custom optical diffusion layers for night-vision readability and emergency operational monitoring in marine control stations.
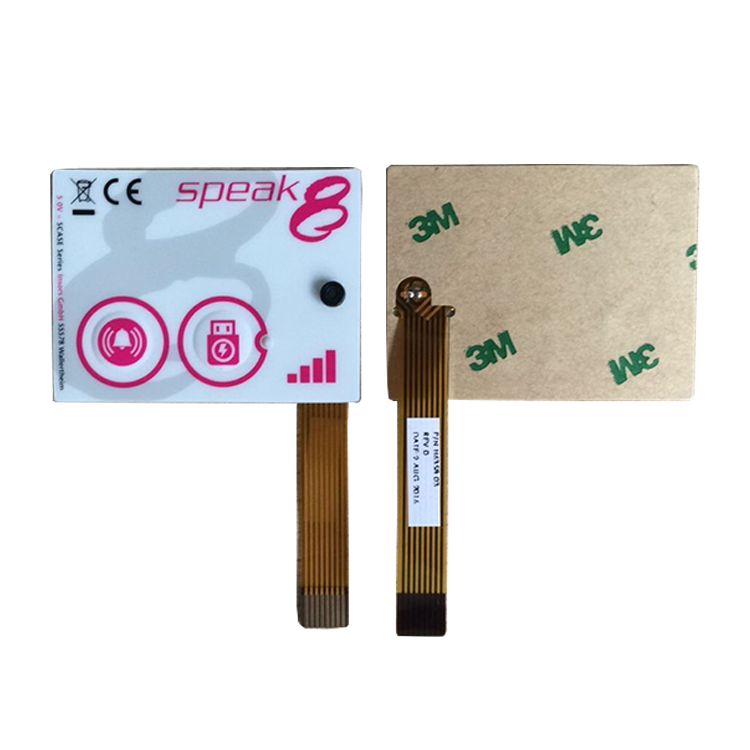
Custom Silk Screen Printed Flexible Thin Film Keypad
Sub-surface graphic printing on premium Autotex XE polyester ensuring text and symbols remain completely immune to abrasive wear and saltwater fading.
Atoll-Resilient Plastic Keypad Architecture: Defeating High Humidity and Airborne Marine Salinity
A technical dissertation on preventing mechanical switch seizure, interfacial delamination, and electrochemical silver dendritic growth in equatorial island environments like Vaiaku, Tuvalu.
Deploying electromechanical user interfaces on Fongafale islet (Vaiaku), Tuvalu presents one of the world's most aggressive environmental stress profiles for electronic equipment. Positioned at 8°31′S latitude in the central Pacific, Vaiaku experiences constant relative humidity averaging between 80% and 95%, year-round ambient temperatures hovering around 28°C to 34°C, intense equatorial Ultraviolet Index ratings (UVI 11+ to 13), and uninterrupted aerosolized marine salt spray carried by prevailing trade winds across the lagoon.
Standard commercial plastic keypad assemblies engineered for temperate indoor deployment fail precipitously under these localized conditions. The primary failure mode observed in remote Pacific atoll infrastructure is hygroscopic silver electromigration. In generic silver-printed polyester membrane circuits, continuous microscopic vapor transmission through standard adhesive boundaries allows moisture to combine with atmospheric chlorine ions. When a DC potential is applied across adjacent switch traces, silver ions dissolve from the positive anode and migrate toward the negative cathode, forming microscopic dendritic whiskers that cause irreversible short circuits.
Carbon Encapsulation & Barrier Chemistry
To neutralize galvanic corrosion and electrochemical dendritic growth, ZIRA implements a proprietary dual-barrier circuit topology. All primary conductive traces are printed using low-resistance, high-purity silver paste, followed immediately by an automated high-density conductive carbon overprint. The carbon overprint completely encapsulates the silver boundary, preventing ionized silver from interfacing with moisture molecules. Furthermore, circuit tails are terminated with selective dielectric cross-over coatings and sealed with hydrophobic polyurethane encapsulation beads.
Hermetic Adhesive Channel Sealing
Adhesive degradation and interfacial delamination represent another catastrophic failure vector in tropical maritime settings. High ambient humidity combined with diurnal thermal expansion breaks down generic pressure-sensitive tapes. We engineer our Vaiaku-bound keypad assemblies utilizing modified high-surface-energy acrylic adhesive matrices—principally 3M™ 300LSE and 3M™ 467MP/468MP. We construct continuous perimeter adhesive gaskets (minimum 3.0mm width) with interior vent channel networks isolated from the external environment, securing IP67 to IP68 hermetic ingress ratings.
Technical Specification Matrix: Standard vs. Marine-Tropical Grade
The comparative data below outlines the material thresholds implemented in ZIRA’s CE-certified plastic keypad and membrane switch assemblies tailored for high-salinity island deployments:
| Engineering Property | Standard Commercial Keypad | ZIRA Tropical Marine Grade (Vaiaku Spec) | Test / Regulatory Standard |
|---|---|---|---|
| Overlay Substrate | Standard Polycarbonate (PC) | Autotex® XE Textured Hardcoat Polyester (PET) | ASTM D3363 (3H Hardness, UV Stable) |
| Ingress Protection | IP40 – IP54 Dust Resistant | IP67 – IP68 Hermetically Perimeter Sealed | IEC 60529 / DIN 40050 |
| Salt Spray Resistance | Seizure / Corrosion at 24 Hours | Passes 96+ Hours continuous neutral salt fog | ASTM B117 / IEC 60068-2-52 Kb |
| Circuit Traces | Bare Silver Ink (Exposed to Air) | Silver Ink with Carbon Barrier Overprint | IPC-TM-650 Electromigration Test |
| Adhesive Lamination | Standard Emulsion Acrylic | 3M 300LSE / 467MP Solvent-Free High Tack | PSTC-101 Adhesion Peel Strength |
| Contact Resistance | < 100 Ω (Fluctuating under dampness) | < 10 Ω (Ultra-stable throughout life cycle) | ASTM F1680 Standard Switch Loop |
| Actuation Lifespan | 100,000 to 500,000 Cycles | 1,000,000 to 5,000,000 Cycles (Metal Dome) | ASTM F1578 Precision Cycling |
Beyond physical ingress prevention, our CE certification dossier verifies full adherence to EMC Directive 2014/30/EU. In atoll installations dependent on low-voltage DC renewable power grids and high-frequency satellite transceivers, our membrane keyboards incorporate integrated aluminum foil or printed conductive carbon-grid shielding layers to eliminate electromagnetic interference (EMI) and electrostatic discharge (ESD) up to 15 kV air discharge.
Mission-Critical Keypad Deployments Across Funafuti Atoll
Examining the specialized human-machine interface requirements of utilities, medical facilities, and maritime installations operating in the administrative capital of Tuvalu.
Solar Microgrid & BESS Controllers (TEC)
Tuvalu Electricity Corporation's ongoing transition toward 100% renewable solar PV and Battery Energy Storage Systems (BESS) relies on inverter control panels that endure high UV index and ambient heat inside outdoor enclosures.
Seawater Reverse Osmosis (SWRO) Desalination
With no freshwater streams and total dependence on rain catchments and SWRO plants in Funafuti, pump controllers and chlorination dosing systems require hermetic IP68 membrane interfaces immune to chemical splashes and brine fog.
Satellite Earth Terminals & Telecom Systems
Tuvalu Telecommunications Corporation (TTC) satellite ground transceivers and microwave links connect Vaiaku to outer islands. Keypads require integrated ESD/EMI shielding preventing signal attenuation and circuit disruption.
Princess Margaret Hospital (PMH) Diagnostic Units
Vaiaku's central hospital depends on durable medical consoles for patient monitors, centrifuges, and diagnostic analyzers that withstand continuous sterilization with sodium hypochlorite and isopropyl alcohol without legend degradation.
Lagoon Vessel Diagnostics & Port Cranes
Marine navigation consoles, VHF radios, and cargo handling gear at Funafuti Deep Sea Port experience direct seawater immersion and intense vibration. Tactile metal dome pushbuttons guarantee tactile confirmation under wet gloves.
Government Meteorological Stations
Tuvalu Meteorological Service climate dataloggers and tidal gauges recording sea-level variations require autonomous low-power HMI panels capable of continuous unattended operation under extreme tropical weather spikes.
Precision Manufacturing Backed by 29+ Years of Engineering Excellence
Established in 1996 in Ningbo, Zhejiang ZIRA Membrane Switch Co., Ltd. provides world-class OEM/ODM production of membrane keypads, silicone rubber buttons, and integrated front panels trusted by multinational conglomerates including ABB and Emerson.
Intertek Onsite Verified Supplier
Our complete manufacturing facilities, cleanrooms, and QA/QC management workflows have been thoroughly verified and audited on-site by Intertek, confirming international legal and technical standing.
End-to-End In-House Tooling & SMT
From laser steel rule dies, embossing matrix CNC carving, precision silkscreen mesh tensioning to high-speed surface-mount component placement, all operations are conducted within our Ningbo plant.
100% Function & Continuity Inspection
Zero defect tolerance. Every membrane keypad passes computerized automated continuity analyzers, contact loop resistance verifiers, insulation resistance meters, and visual colorimetric inspections.
Global Multimodal Logistics Network
Over 50% of our output serves global export markets across Oceania, North America, and Europe. We provide FOB, CIF, DDP, and rapid air courier dispatches via Suva routing into Funafuti.
Flexible Engineering MOQ (1 pc to 100k+)
We empower localized engineering teams and pilot projects with low minimum order barriers. Functional prototypes from 1 piece with comprehensive DFM design reviews prior to volume manufacturing.
Tier-1 Brand Supplier Reputation
Demonstrated track record maintaining supplier qualification standards for ABB, Emerson, and international healthcare instrument OEMs, backed by full traceability files and certificates of conformance.
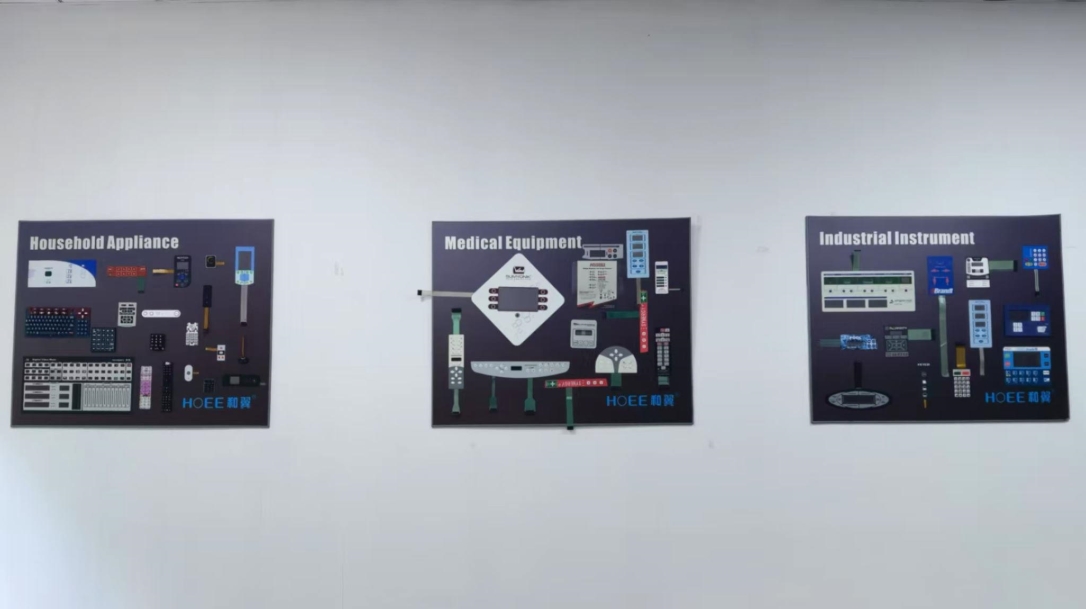
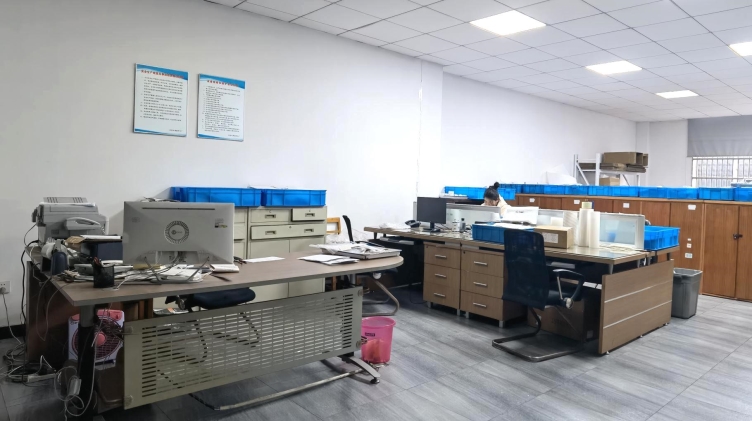
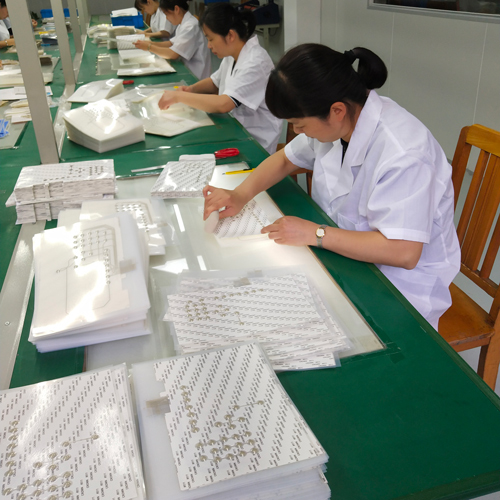
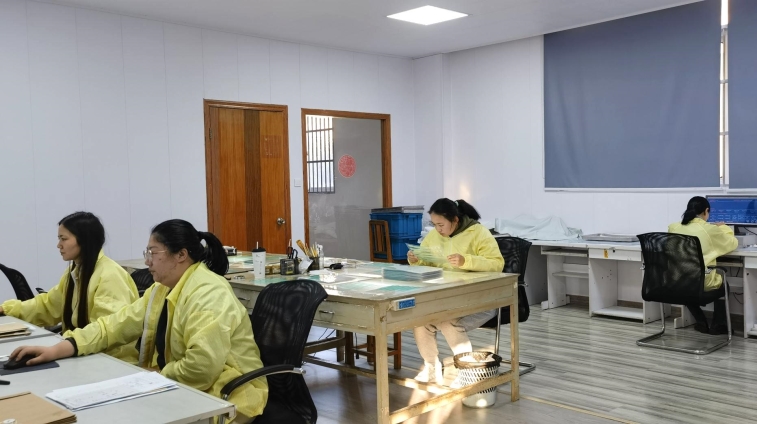
Inside ZIRA’s Precision Manufacturing & Testing Facility
Real photographic records of our production floor, cleanrooms, and testing facilities in Ningbo, Zhejiang.
Future HMI Engineering Trends Shaping Tuvalu’s Industrial Procurement
Anticipating the technological shifts in materials, optics, and human-machine interaction relevant to Pacific Island infrastructure modernization.
Low-Power Light Guide Film (LGF) Integration
As remote Pacific atolls transition toward autonomous off-grid solar-plus-storage energy, peripheral electrical loads are intensely scrutinized. Standard multi-LED backlit keypads that consume hundreds of milliamps are rapidly being replaced by micro-etched Light Guide Films (LGF). LGF channels illumination uniformly across extensive key layouts using only 2 to 4 ultra-low-current side-firing SMT LEDs, slashing thermal dissipation and parasitic battery draw while maintaining crystal-clear nocturnal legibility.
Transition to Capacitive ITO Touch with Water Rejection
While tactile metal domes remain crucial for heavy maritime gear, stationary utility panels in Funafuti are transitioning toward solid-state Capacitive Indium Tin Oxide (ITO) touch film assemblies. With zero moving parts, capacitive switches eliminate mechanical fatigue completely. By integrating tuned microcontroller firmware with sophisticated water-rejection algorithms, modern capacitive panels operate flawlessly even when covered with conductive saltwater droplets or dew condensation.
High MTBF Architecture to Eliminate Air-Freight Costs
Given that shipping replacement components to Tuvalu entails high international logistics expenditures and lengthy customs transit times via Fiji, procurement authorities are moving away from low-cost throwaway keypads. The prevailing trend favors total lifecycle return on investment: specifying military-grade stainless steel domes (5 million switch actuations), cross-linked silicone keymats, and thick hard-coated polyester films that ensure decade-long operational continuity without field failure.
Frequently Asked Questions for Vaiaku & Pacific Buyers
Essential information on technical parameters, compliance documentation, shipping logistics, and custom manufacturing minimums for Tuvalu procurement managers.
We regularly export custom HMI assemblies to Pacific Island nations. For rapid prototyping and urgent critical replacement orders, we ship directly via international express air couriers (DHL/FedEx) connecting through Auckland or Nadi into Funafuti International Airport (FUN). For standard volume orders, sea freight is consolidated at Ningbo Port and dispatched to Suva, Fiji, where it connects with regional feeder cargo vessels docking at Funafuti Port. We accommodate EXW, FOB Ningbo, CIF Funafuti, and DDP Incoterms.
Every customized keypad production run comes accompanied by a full CE Declaration of Conformity (DoC) proving adherence to the European Electromagnetic Compatibility (EMC) Directive 2014/30/EU and RoHS Directive (EU) 2015/863. For assemblies featuring integrated backlighting or high-density SMT components, we provide laboratory test reports verifying electromagnetic immunity and electrostatic discharge thresholds (IEC 61000-4-2 standard) to satisfy Tuvalu customs and donor agency audit guidelines.
Yes. Reverse engineering of legacy front panels and defective membrane switches is one of our key service offerings. If original Gerber or CAD files are unavailable, clients in Vaiaku can ship a physical sample (even a non-functional or cracked switch) or provide a calibrated flatbed scan with schematic pin-out notations. Our R&D engineering department reconstructs the dimensional layout, matches the exact Pantone/RAL surface pigments, routes the trace matrix, and delivers 3D/2D engineering drawings for client sign-off within 48 to 72 hours.
In aggressive atoll environments like Vaiaku, exposed metal contacts quickly develop green verdigris or insulating chloride films. We strongly recommend specifying female female crimp connectors with polarizing friction latches housed in PBT bodies (such as Nicomatic or Amphenol FCI 2.54mm pitch connectors), accompanied by gold-plated contact terminals. Where Zero Insertion Force (ZIF) tails are necessary, we apply selective carbon overprinting on the contact fingers and encapsulate the tail transition zone in UV-cured resin.
Recognizing that municipal utilities and maritime operators in Funafuti often need small batch runs for critical maintenance rather than tens of thousands of units, our minimum order quantity starts from just 1 to 5 pieces for initial engineering evaluation. Standard sample lead times are typically 7 to 10 working days following artwork and circuit sign-off. Repeat volume production batches (100 to 5,000+ units) are manufactured and packaged in vacuum-sealed anti-static nitrogen barrier pouches within 12 to 18 working days.
Our in-house QA laboratories utilize calibrated cyclic corrosion chambers executing ASTM B117 and IEC 60068-2-52 Kb Severity 2 test protocols. Keypad assemblies undergo 96 to 168 hours of continuous exposure to a 5% NaCl aerosol solution atomized at 35°C, followed by damp heat storage phases at 93% relative humidity. Only materials that demonstrate zero edge peeling, zero conductive trace resistance drift, and zero loss of tactile dome click ratio are cleared for Pacific regional delivery.
Request a DFM Engineering Review for Your Vaiaku Project
Whether you are engineering a custom solar inverter interface, upgrading reverse osmosis desalination controls, or manufacturing ruggedized marine electronics for Tuvalu and the South Pacific, ZIRA’s engineering team provides material stack-up recommendations, rapid CAD reviews, and competitive factory-direct quotations within 24 hours.
